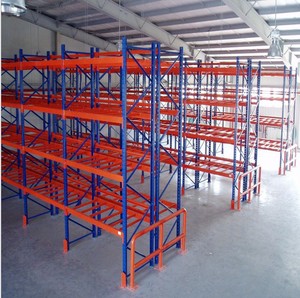
Heda Automated Warehouse Pallet Runner Radio Shuttle Rack
Deep-lane semi-automated dynamic racking built for chilled and sub-zero storage with seamless FIFO/LIFO execution.
Engineered for mission-critical material handling, maximum footprint optimization, and demanding temperature-controlled or heavy-load distribution environments.
Deep-lane semi-automated dynamic racking built for chilled and sub-zero storage with seamless FIFO/LIFO execution.
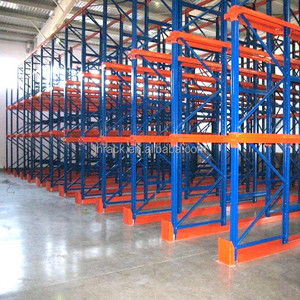
Aisle-free structural framework configured for mass volume SKU batching, maximizing vertical clearance and structural rigidity.
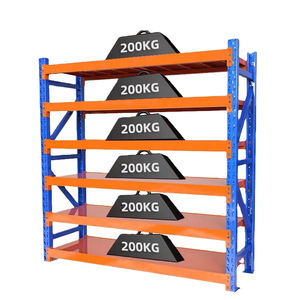
Reinforced uprights engineered to accommodate variable pallet configurations with reinforced column bases for forklift impact resistance.
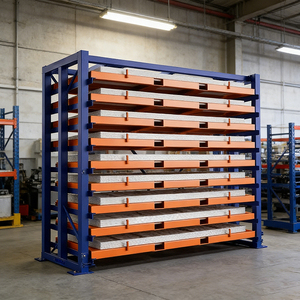
Ergonomic drawer mechanisms and cantilever extensions tailored for sheet steel, heavy dies, and industrial fabrication materials.
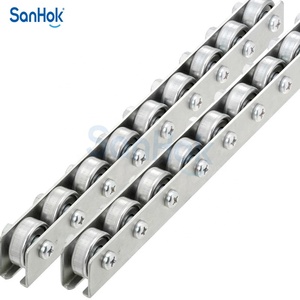
Continuous dynamic flow beds optimized for low-friction picking lanes, order staging zones, and strict FIFO replenishment.
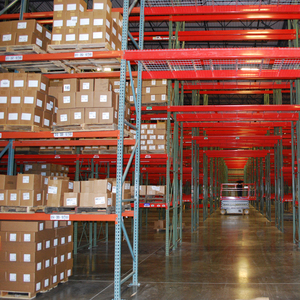
Precision barcode integration, systematic load labelling, and aisle layout design for seamless WMS track-and-trace alignment.
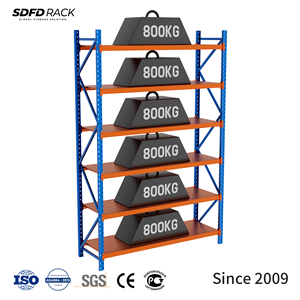
100% immediate pallet selectivity engineered with 75mm/50mm pitch increments for dynamic multi-SKU FMCG facilities.
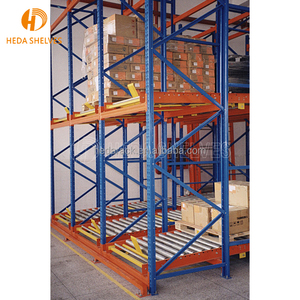
Ergonomic split-case and carton handling solution equipped with durable nylon or metallic roller tracks for rapid e-commerce pick faces.
Direct manufacturer capabilities eliminate intermediary overheads, ensure rigorous metallurgical quality control, and offer rapid sea-freight connectivity across global transport corridors.
Every structural column, load beam, and mobile base carriage is engineered under EN 15512 and ISO standards (Certificate No. 18624Q00169R0M, CE No. 2435-CPR-8605159). Our documentation stands up to the scrutiny of municipal building inspectors, international third-party engineering auditors, and insurer loss-prevention teams.
Operating in tropical, sub-tropical, or cold storage conditions demands advanced chemical surface conditioning. We utilize comprehensive multi-stage acid pickling and phosphating pre-treatments followed by electrostatically applied thermo-hardened epoxy polyester powder coats. Hot-dip galvanization is available for sub-zero freezer floors and corrosive industrial environments.
Our in-house design office provides full CAD floorplans, 3D BIM clash-detection models, and finite element structural calculations free of charge. For active seismic regions, such as the Philippines, Indonesia, and Japan, our structural team models dynamic load accelerations, engineering oversized reinforced baseplates and specialized back-to-back bracing configurations.
A data-backed look at how mobile base and semi-automated racking systems resolve spatial constraints across modern fulfillment centers.
| System Typology | Footprint Utilization | Direct SKU Selectivity | Cold Chain Energy Conservation | Forklift Cycle Efficiency | Optimal Application Scenario |
|---|---|---|---|---|---|
| Movable Pallet Racking (Mobile Base) | 85% – 90% (Single moving aisle) | 100% (Individual aisle opening) | Exceptional (Downsizes freezer volume by 45%) | Moderate (Requires motorized aisle traversal) | Cold storage, spare parts, archive repositories |
| Automated Radio Shuttle | 80% – 85% (Continuous deep lane) | Batch / Lane Dependent (FIFO/LIFO) | Superior (Uninterrupted thermal density) | High (Cart runs independently inside lane) | High-throughput FMCG, beverages, dairy processing |
| Selective Pallet Racking (Standard) | 35% – 40% (Multiple dedicated aisles) | 100% (Instant simultaneous access) | Low (Heats or chills empty corridor space) | High (Instant reach, zero automated delay) | Third-party multi-tenant 3PL warehouses |
| Drive-In / Drive-Through System | 65% – 75% (Aisle reduction design) | Low (Last-In-First-Out batch control) | Good (High cubic density, reduced airflow) | Moderate (Vehicle must physically enter rack bay) | Raw material staging, seasonal agriculture bulk |
The global intralogistics landscape is experiencing structural disruption. As industrial real estate values climb and supply chains embrace IoT, movable pallet racking procurement is pivoting around three core innovations.
Thermal loss inside industrial freezers represents an ongoing operational expense. Movable pallet racking enables warehouse operators to cut cubic meter refrigeration requirements by roughly 40% to 50% for equivalent pallet counts. Specifiers are targeting low-draw variable frequency drive (VFD) motors, regenerative braking integration, and optimized airflow channel profiles to hit corporate carbon neutrality targets.
Modern mobile racks are no longer standalone mechanical assemblies. Advanced systems feature multi-aperture photoelectric safety curtains, ultrasonic obstruction detectors, and programmable logical controllers (PLC) that communicate over industrial Ethernet or private 5G networks directly with WMS/WCS platforms. These integrations facilitate automated night-parking configurations, scheduled fire-protection spacing, and remote health diagnostics.
The boundary between stationary steel racks and autonomous mobile robotics is blurring. Leading facilities are implementing hybrid architectures where automated guided vehicles (AGVs) or AMRs interact with motorized mobile carriages. Intelligent aisle clearance signals alert mobile robots before approach, transforming traditional dense storage blocks into fully automated, lights-out distribution hubs without costly high-bay construction.
From prime Q235B/Q355B cold-rolled steel coils to ocean-container transport, our 10-stage in-house production line eliminates sub-supplier defects.
Spectrometric assay & tensile verification on incoming coils.
High-tolerance automated longitudinal strip cutting.
Continuous CNC hole stamping with consistent pitch accuracy.
Multi-stand cold rolling ensuring beam cross-section stability.
Shielded dual-torch automated weld joints on load-bearing brackets.
Shot-blasting to eliminate scale, burrs, and oxidation.
Chemical pre-treatment bath for superior molecular coat bonding.
Powder polymer baking at 180°C–200°C for wear protection.
Deflection load tests and weld penetration ultrasonic inspection.
Protected steel bundling engineered for container utilization.
Direct technical answers addressing engineering constraints, slab requirements, safety standards, and project commissioning.
Send your warehouse architectural drawings, pallet load specifications, and forklift fleet parameters to our Guangzhou project design center. Receive a custom 2D layout, 3D visualization, and structural load analysis within 24 hours.
Inquire Now