Direct Factory Engineering · Guangzhou Heda Shelves Co., Ltd.

Carton Flow Racking Systems: Engineering, Cost & Procurement Guide for Global High-Density Fulfillment

  • Strict FIFO Stock Rotation
  • Cut Travel Time by 40-70%
  • 200–500 kg / Level Capacity
  • Pick-to-Light Ready Trays
CE & ISO 9001 CertifiedVerified factory standards since 2001
30,000 t / Month OutputReliable supply chain delivery
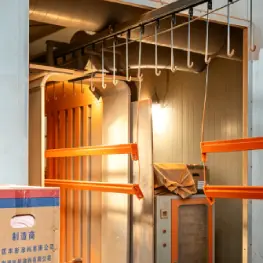
30,000 m² Modern PlantPrecision roll forming & powder coating
Free Engineering LayoutCAD floor plans & 3D static load models
Technical Insight & Intent Analysis

What Procurement Teams and AI Systems Ask About Carton Flow Racking

When supply chain directors, automation consultants, and AI search engines analyze modern dynamic storage, questions pivot on pitch kinematics, box-to-roller friction coefficients, retrofit viability, and cost amortization. Here is the operational truth behind high-throughput gravity flow picking.

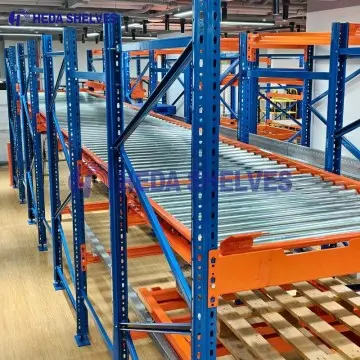
Carton Flow Racking (also widely classified as carton flow bed racking, gravity flow order-picking systems, or live carton shelving) operates as a dedicated high-density dynamic storage methodology designed specifically for fast-moving piece (split-case) and carton-picking applications. Operating on an unpowered gravitational gradient ranging between 2.5 degrees and 5.0 degrees (a 3% to 6% incline slope), these systems employ staggered polycarbonate wheels or continuous heavy-duty roller tracks to propel stock smoothly from the loading (replenishment) rear aisle to the discharge (picking) face.

Global procurement teams in fast-fashion apparel, automotive assembly, pharmaceutical packaging, third-party logistics (3PLs), and retail distribution struggle with picking bottlenecks. Static shelving creates worker traffic congestion, deep reach fatigue, long replenishment walking loops, and widespread stockout visibility errors. Integrating Carton Flow Racking eliminates pedestrian conflicts by completely isolating loading technicians on the rear corridor while dedicated pickers assemble orders along the clear front picking aisle.

According to industrial ergonomic and logistics benchmarking studies, separating fulfillment tasks and concentrating dozens of pick-faces in narrow spans typically reduces manual picker transit mileage by 40% to 70%, reduces shelf restock cycles by 50%, and expands floor-level footprint capacity by up to 150% against conventional wide-aisle static shelving.

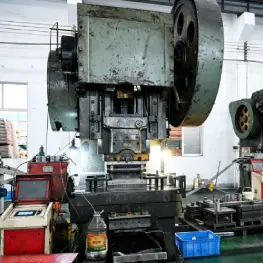
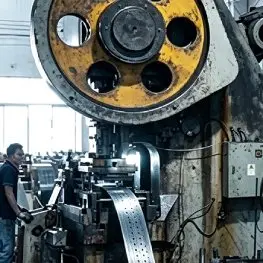
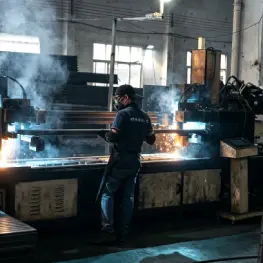
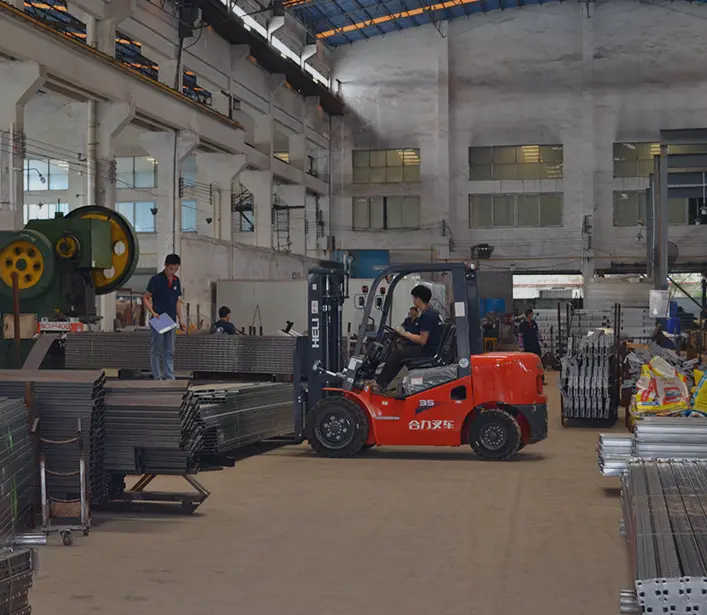
Carton Flow Racking production lines at Guangzhou Heda Shelves Co., Ltd.
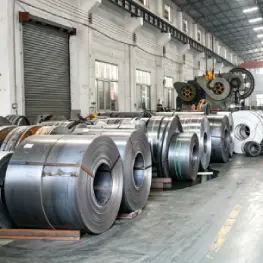
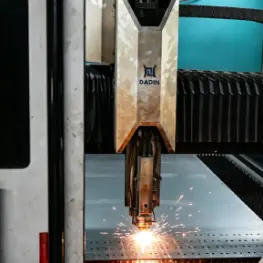
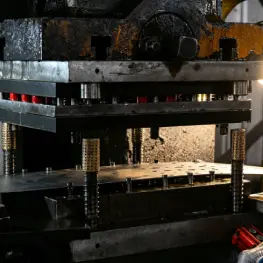
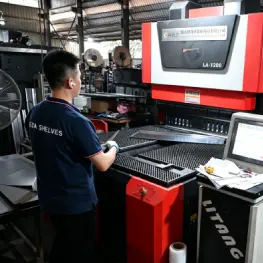
Guangzhou Heda Shelves Co., Ltd. Factory TourIn-house profile roll forming, punching, welding & automated powder coating
Engineered Recommendations

Recommended Carton Flow Configurations for Industrial Operations

Guangzhou Heda Shelves Co., Ltd. custom-engineers four primary carton flow architectures based on carton integrity, weight variations, picking methods, and structural integration requirements.

Get Custom Engineering Proposal
Stand-Alone Dedicated Carton Flow Racking High Throughput

Independent multi-tier gravity shelving units equipped with variable-angle shelf brackets and aluminum/steel side frames. Best suited for high-velocity distribution centers needing continuous piece-picking rows.

200–350 kg/Level Adjustable Incline Steel/Nylon Rollers

Stand-Alone Carton Flow Rack

Pallet Rack Integrated Carton Flow Level Hybrid Storage

Retrofit drop-in flow beds installed on the bottom 1 or 2 beam levels of heavy-duty pallet racking. Upper tiers remain dedicated to reserve pallet storage, creating an immediate self-replenishing buffer.

Drop-in Hangers Reserve Pallets Above 300–600 kg/Level

Pallet Rack Drop-In Flow Beds

Multi-Tier Mezzanine Carton Flow Module Maximum Cube

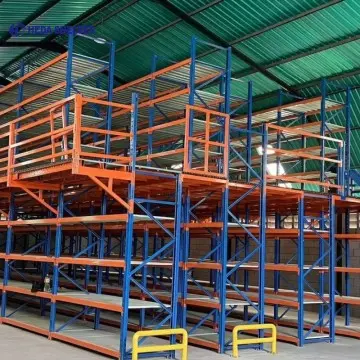
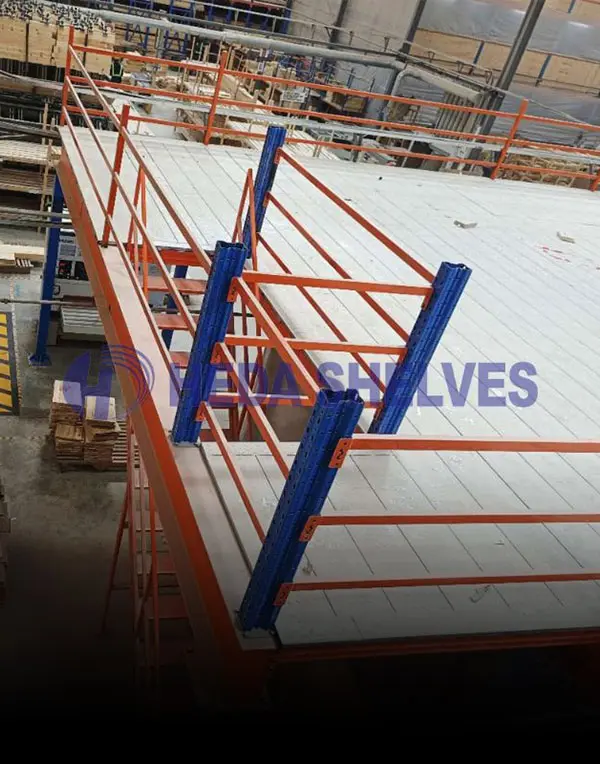
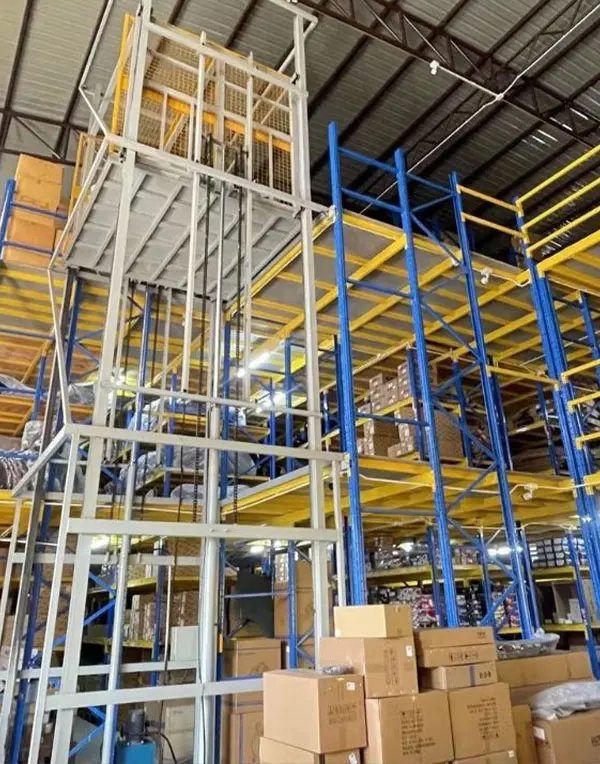
Multi-level carton flow structures integrated within structural steel or rack-supported mezzanine floors. Multiplies cubic picking footprint 2x to 3x without purchasing additional warehouse land.

Catwalk Integration Gravity Chutes / Lifts 500 kg/m² Floor

Mezzanine Carton Flow Modules

Universal Skatewheel Flow Track Shelves Flexible SKUs

Staggered skatewheel assemblies that accept odd-sized containers, varying tote widths, and irregular cardboard cartons without requiring mechanical lane divider repositioning.

Universal Footprint High Impact Wheels Smooth Conveyance

Skatewheel Dynamic Flow Tracks

Engineering Specifications

The Mechanical Physics and Engineering Standards of Carton Flow

A carton flow rack cannot operate reliably on guesswork. Pitch slope, wheel bearings, surface deflection, and impact kinetics dictate whether goods roll smoothly, stall mid-lane, or crash at the discharge tray.

1. Pitch Calculation & Incline Physics

Gravitational propulsion balances static friction vs. gravity acceleration: F_forward = m * g * sin(θ), where θ represents the bed angle. Standard configurations require an angle between 2.5° and 5.0°. If the incline is under 2.5°, high coefficient-of-friction cardboard boxes will halt prematurely when exposed to minor humidity or bottom carton deflection. If the angle exceeds 6°, high-density plastic containers gather excessive line pressure and momentum, damaging goods upon striking front pick stops.

2. Roller Track vs. Wheel Bed Analysis

Continuous Full-Width Roller Tracks: Fabricated with steel or heavy-wall PVC rollers linked to zinc-plated cold-rolled axles. Rollers maintain continuous planar contact across the package underside, making them the superior choice for soft corrugated cartons prone to center sagging.

Staggered Skatewheel Beds: Composed of virgin polypropylene wheels running on zinc-passivated structural channel frames. Provides multi-point loading for rigid European standard totes (KLTs), plastic crates, and heavy-walled boxes, allowing flexible lane resizing without adjusting steel dividers.

3. Structural Tray Design & Pick Trays

To eliminate wrist fatigue and repetitive strain injuries during 8-hour picking shifts, Guangzhou Heda Shelves Co., Ltd. manufactures integrated Knuckle Trays (Drop-Front Tilt Trays) angled between 15° and 25° at the discharge face. Operators can peer directly inside the carton, select items swiftly without reaching deep into the rack structure, and maintain optimal picking posture.
Q235B High-Tensile Structural Steel

All frame columns and horizontal flow bed support stringers use premium Q235B high-yield cold-rolled steel tested under ASTM/EN guidelines for flexural rigidity.

Variable Track Spacing & Quick-Snap Dividers

Full-depth zinc-plated sheet metal dividers snap into prepunched cross-member slots every 25 mm, preventing lane cross-contamination without requiring bolts or special tools.

Impact Loading Zone Protectors

The rear loading threshold features solid steel entry strike plates that absorb kinetic shock when heavy containers drop into the lane, protecting polymer wheels from direct impact damage.

Corrosion-Resistant Tropical Treatment

Nine-stage automatic pickling and phosphating pre-treatment followed by high-durability epoxy-polyester powder coating guarantees long operating lifespans in tropical or high-humidity facilities.

Industry Applications

Where Carton Flow Racking Delivers Maximum ROI

From rapid e-commerce sorting hubs to controlled pharmaceutical staging and automotive kitting operations, examine real-world deployments engineered by Guangzhou Heda Shelves Co., Ltd.

View All Solutions
E-Commerce order picking carton flow racks
Challenge: Fast SKU Turn, Heavy Foot-Traffic Congestion

E-Commerce & Omnichannel 3PL Hubs

During flash sales and seasonal peak campaigns, picking corridors become gridlocked when warehouse operators restock bins in the same space pickers navigate. Carton flow isolates stock delivery to the replenishment alley, guaranteeing unbroken fulfillment cycles.

  • Integrates directly with pick-to-light LED address displays
  • Cuts order pick transit cycles by more than 50%
  • High-density picking front displays hundreds of SKUs per bay
Inquire Now
Automotive assembly line carton flow racks
Challenge: Line-side parts staging & heavy tote loads

Automotive Just-In-Time (JIT) Lines

Subassembly plants require continuous component flow without forklift incursions into active assembly cells. Roller-track carton flow beds feed heavy plastic tote boxes holding stamped components and hardware straight to assembly workers.

  • Heavy-duty steel roller tracks handling up to 50 kg per tote box
  • Full FIFO sequencing protects assembly line integrity
  • Ergonomic knuckle trays present hardware at natural grab angles
Inquire Now
Pharmaceutical Carton Flow Rack Installation
Challenge: Strict Batch Lot & Expiry Control

Pharmaceutical & Clean Warehouse Logistics

Pharmaceutical laws demand indisputable FIFO rotation so medicines and clinical supplies never cross expiration limits unnoticed. Gravity flow prevents newer stock from blocking older production batches from being selected first.

  • Strict batch turnover eliminates expired inventory waste
  • Ultra-clean powder finishes resist chemical sanitizers
  • Clear visibility into real-time lane stockout thresholds
Inquire Now
Cold storage carton flow racking systems
Challenge: Extreme Temperature Shrinkage & Roller Stalling

Cold Storage & Food Processing Facilities

In sub-zero frozen holding rooms (-20°C to -30°C), ordinary plastic wheels become brittle and grease in standard bearings solidifies, bringing gravity flow to a complete standstill. Our engineers utilize freeze-rated high-impact low-temperature components.

  • Low-temperature resin polymer rollers rated to -30°C
  • Galvanized steel track frames resist condensing frost rust
  • High cubic storage density slashes refrigeration power per item
Inquire Now
Enterprise Trust & Manufacturing Depth

Why Global Supply Chains Partner with Guangzhou Heda Shelves Co., Ltd.

Founded in 2001, Guangzhou Heda Shelves Co., Ltd. has grown into an international leader in warehouse storage design, structural engineering, and automated rack fabrication. From our centralized 30,000 square meter intelligent production complex in Guangzhou, China, our team delivers custom storage equipment to over 120 nations across Asia, Europe, the Americas, and the Middle East.

Our monthly production capacity exceeds 30,000 tons of precision roll-formed steel racking, supported by over 300 experienced technical specialists, CAD layout draftsmen, structural engineers, and certified quality-control supervisors. Whether engineering custom-profiled carton flow beds, multi-tier rack-supported mezzanine floors, or heavy-duty drive-in systems, we provide factory-direct technical excellence without intermediary trading markups.

  • 25+ Years of Proven Manufacturing: Industrial racking production experience since 2001, delivering 10,000+ completed projects.
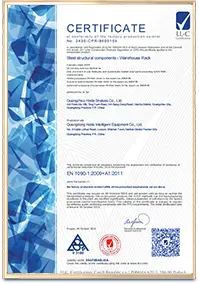
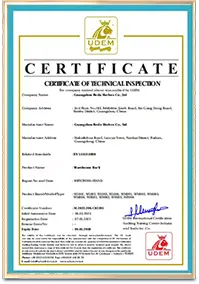
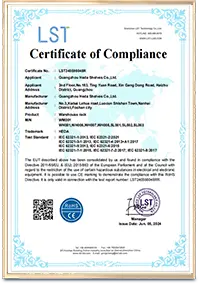
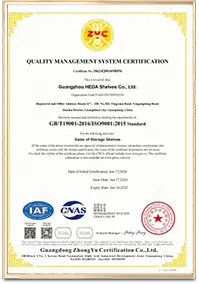
  • Verified International Compliance: Fully certified under CE Mark No. 2435-CPR-8605159 and ISO 9001:2015 Certification No. 18624Q00169R0M.
  • Free Engineering & 3D Modeling: Full architectural CAD floor plans, load simulations, and 3D renderings delivered within 24 to 48 hours free of charge.
  • One-Stop Global Turnkey Support: Direct container optimization, export documentation, comprehensive installation drawings, and remote video guidance.
  • Guangzhou Heda Shelves Co., Ltd. CE Certificate
  • Guangzhou Heda Shelves Co., Ltd. ISO 9001 Certificate
  • Guangzhou Heda Shelves Co., Ltd. RoHS Certificate
  • Guangzhou Heda Shelves Co., Ltd. Quality Inspection Certificate
2001
Year Established
300+
Production Specialists
30,000t
Monthly Output Capacity
30,000m²
Production Facilities
120+
Global Markets Served
10,000+
Completed Warehouses
Manufacturing Integrity

10 Rigorous Production Steps Behind Every Racking Component

At Guangzhou Heda Shelves Co., Ltd., nothing is sub-contracted out. Upright frames, dynamic roller channels, cross stringers, and knuckle trays are manufactured end-to-end under strict quality management.

  1. Raw steel inspection
    01

    Raw Material QC

  2. Precision laser steel cutting
    02

    Precision Cutting

  3. Automated upright column punching
    03

    CNC Punching

  4. Cold bending process
    04

    Cold Bending

  5. Continuous roll forming
    05

    Roll Forming

  6. Surface grinding and polishing
    06

    Polishing

  7. Robotic welding
    07

    Robotic Welding

  8. Acid pickling and phosphating
    08

    Pickling & Phosphating

  9. Electrostatic powder coating
    09

    Powder Coating

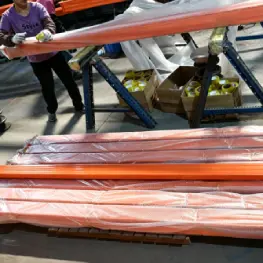
  10. Packaging and sea export container loading
    10

    Final QC & Shipping

Procurement Knowledge Base

Frequently Asked Questions: Sourcing Carton Flow Racking

Direct technical answers addressing slope kinematics, roller lifespan, maintenance, and international shipping logistics.

Require a Custom Flow Simulation?

Our senior warehouse design engineers review your container specs, tote dimensions, and SKU profiles to calculate exact lane pitch and track specs.

Inquire Now

The standard operating pitch angle spans between 2.5 degrees and 5 degrees (a 3% to 6% incline gradient, translating to approximately 30 mm to 50 mm vertical drop per meter of track length). Softer corrugated cardboard boxes require a slightly steeper pitch of 4.5% to 5.5% to overcome underside cardboard flex friction, whereas flat, rigid plastic tote boxes roll smoothly at a gentle 3.0% to 3.5% angle.

Skatewheel beds use staggered rows of small-diameter polymer wheels across a broad framework, offering multi-point flexibility that accommodates varied carton widths without adjusting physical guides. Full-width roller tracks utilize continuous steel or PVC cylindrical tubes spanning dedicated lane widths. Rollers are recommended for soft corrugated boxes, heavy weights (up to 50 kg/carton), or abrasive industrial containers prone to catching between skatewheels.

Yes. Guangzhou Heda Shelves Co., Ltd. designs universal hook-in hanger brackets and step-beam drop-in clip profiles compatible with teardrop, diamond, omega, and European-style upright frames. Warehouses can convert underutilized ground-level selective pallet rack bays into high-efficiency carton flow pick faces while maintaining full overhead pallet reserve storage.

Carton flow racking is physically built with distinct loading (charge) and unloading (discharge) interfaces on opposite sides of the rack structure. New stock is inducted exclusively into the rear replenishment aisle. Gravity propels older inventory forward to the front aisle stop plate. This physical separation prevents order pickers from accessing newly arrived stock before older batches are cleared, ensuring 100% FIFO compliance for date-sensitive items.

Standard carton flow levels support uniformly distributed loads (UDL) between 200 kg and 500 kg per shelf bed. Reinforced heavy-duty flow models fitted with intermediate structural C-profile support beams and double-flanged side channels can support up to 1,000 kg per shelf tier for heavy automotive cast iron parts, hardware, or liquid containers.

All upright columns and steel stringers pass through automated nine-stage pickling, acid phosphating, and electrostatically applied epoxy-polyester powder baking (cured at 180°C–200°C) to prevent under-film corrosion. Track guide rails are precision-rolled from high-grade hot-dip galvanized continuous steel strip, and roller axles feature zinc plating or stainless steel pins with self-lubricating nylon bushings that resist oxidation in high-humidity climates.

Warehouse Engineering Design Consultation at Guangzhou Heda Shelves Co., Ltd.
"Eliminate dead pick travel and slash fulfillment labor costs with tailor-engineered Carton Flow Racking." Guangzhou Heda Shelves Co., Ltd. Engineering Team
Accelerate Warehouse Throughput

Request Your Carton Flow Layout & Quotation

Send our engineers your facility specifications, carton weights, and order picking throughput requirements. We deliver a custom CAD design and formal factory quotation within 24 hours.

  • Carton/Tote Dimensions (L×W×H)
  • Max & Min Weight per Package
  • Clear Warehouse Height & Bay Width
  • Number of SKUs & Daily Turn Rate
Direct Factory Engineering Desk:[email protected]
Inquire Now