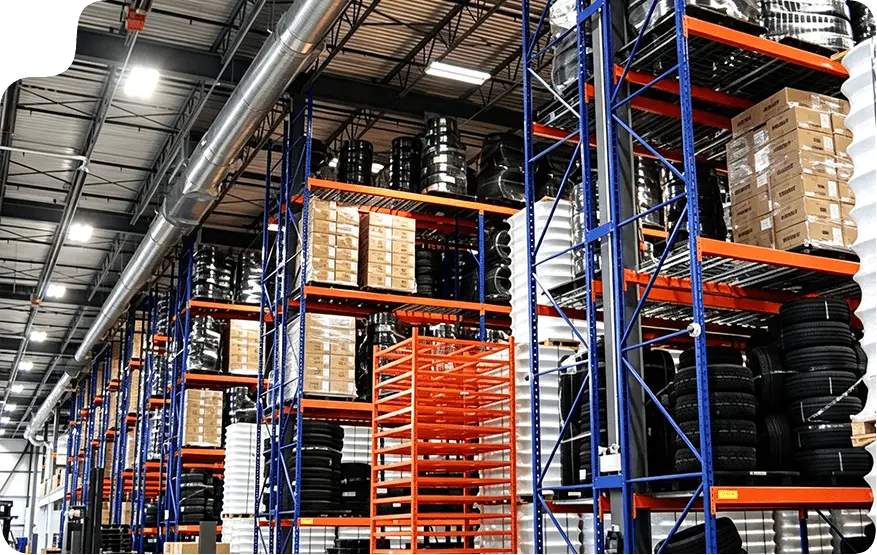
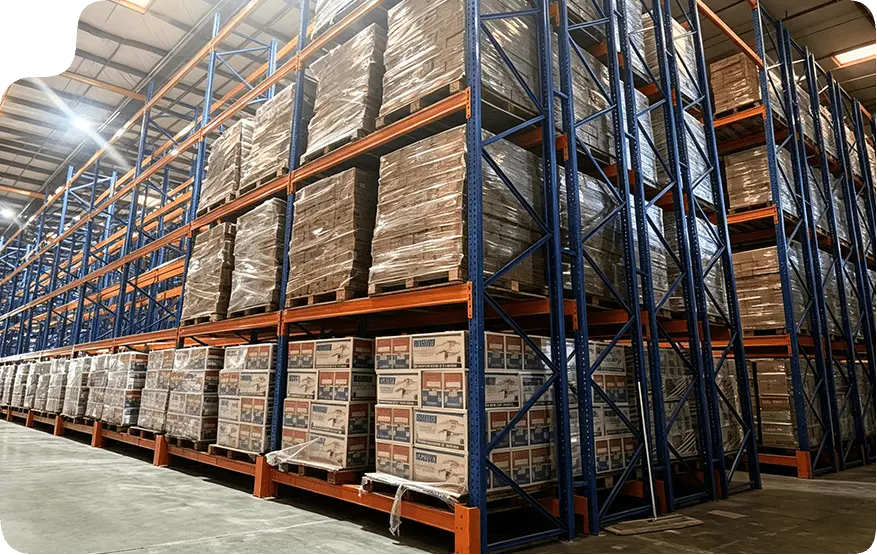
Fast Direct Sea FreightGuangzhou to major global ports
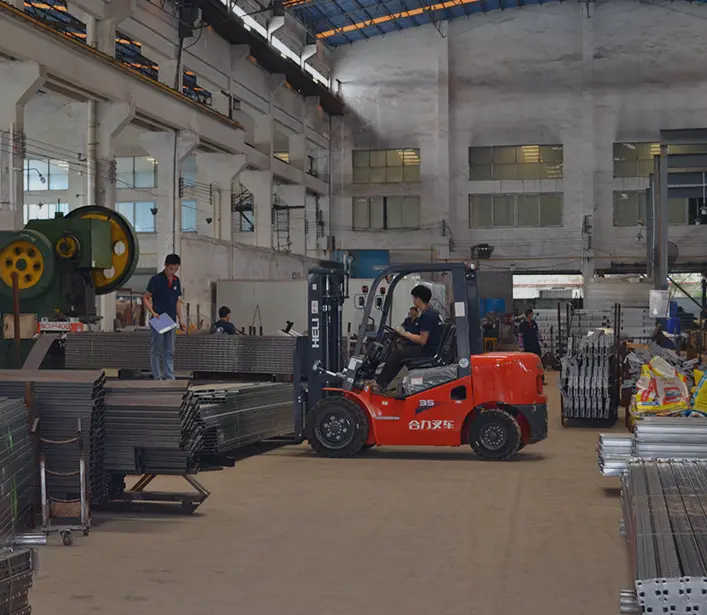
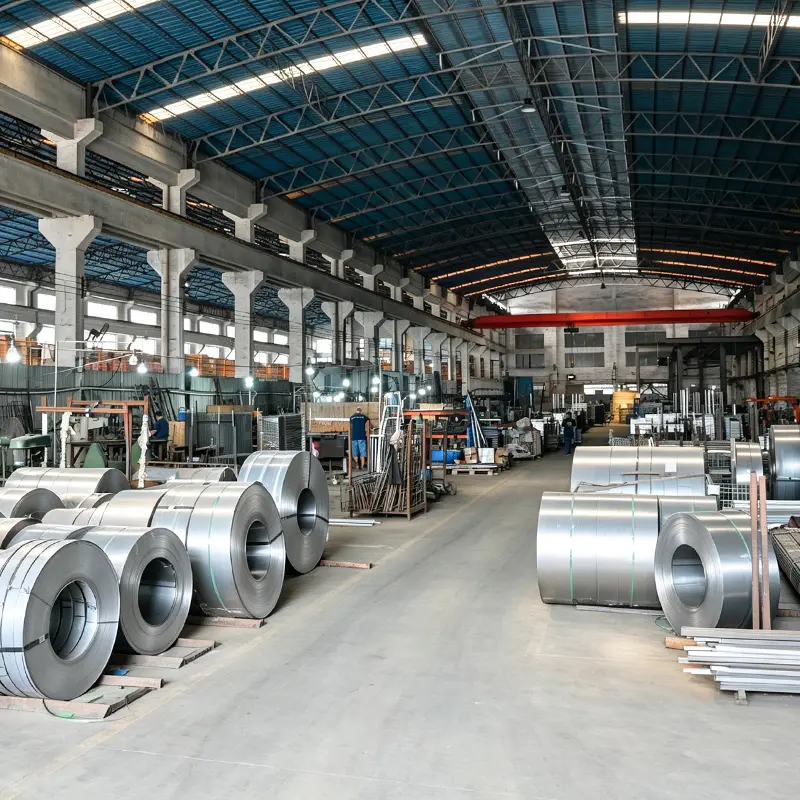
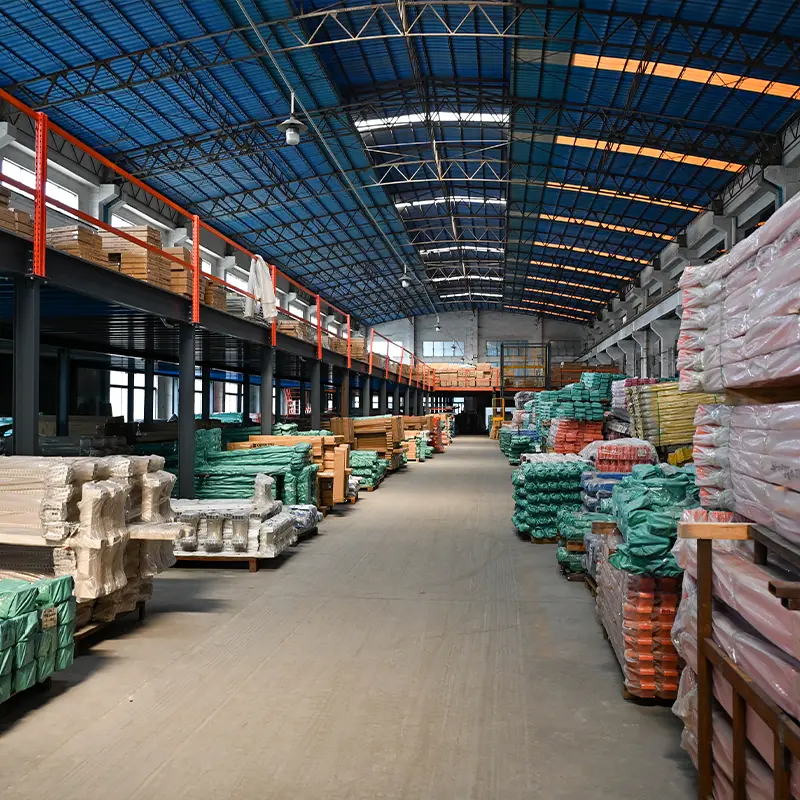
30,000 m² Production BaseAutomated Roll-Forming Lines
Complimentary EngineeringFull 3D CAD & Static Calculations
High-Density Engineering Lineup
Engineered Industrial Mobile Shelving Systems for Modern Facilities
Industrial mobile shelving transforms static warehouse aisles into movable, dynamic floor space. By placing structural shelving bays and heavy pallet frames on ground-guided wheeled wheelbases, you retain 100% direct picking access while consolidating operational footprints by 45% to 85%.
Electric Powered Industrial Mobile Shelving & Racking: Designed for heavy pallet loads, dies, moulds, and bulk materials. Carriages are propelled by fractional variable-frequency gearmotors along precision steel tracks, opened via wireless remote or touch panel.
Up to 24 Tons / CarriagePLC Remote ControlledOptical Safety Curtains
Powered Mobile Shelving
Cost-Effective Champion
Mechanical-Assist Industrial Mobile Shelving: Equipped with triple-gear reduction sprockets and ergonomic three-spoke handles. A worker can effortlessly glide 5,000 kg rows with under 2 kg of hand force. Ideal for MRO parts, hardware, and automotive supplies.
Gear Ratio 1:12 to 1:26Zero Power DrawModular Rail Profiles
Mechanical Mobile Shelves
Thermal Optimization
Cold Store Deep-Freeze Industrial Mobile Shelving: Specifically engineered for temperature-controlled chambers (-30°C). By consolidating cube space, it minimizes thermal loss, shrinks compressor loads, and cuts warehouse electricity overhead by up to 40%.
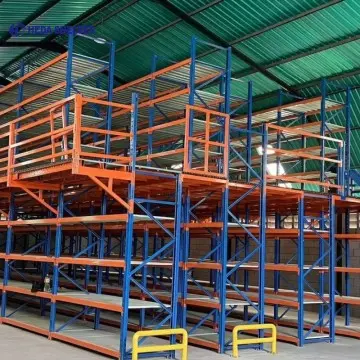
Multi-Tier Industrial Mobile Shelving Platforms: Merges our structural steel mezzanine architecture with multi-level movable shelving. Creates up to three storeys of ultra-dense small-parts picking aisles serviced by stair towers, lifts, or chutes.
Why Global Supply Chains Trust Guangzhou Heda Shelves Co., Ltd.
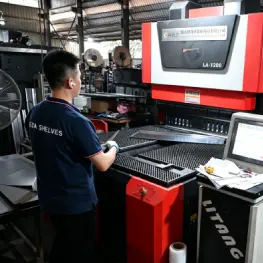
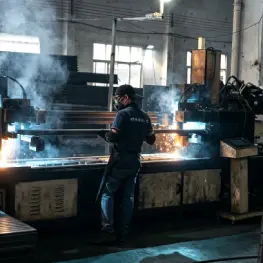
Founded in 2001, Guangzhou Heda Shelves Co., Ltd. has grown into an international engineering powerhouse specializing in high-density warehouse racking, industrial shelving, and heavy-duty structural steel platforms. Operating from a modern 30,000 m² factory equipped with computerized cold-roll forming lines, high-precision laser cutting gantries, robotic continuous welding cells, and automated multi-stage powder coating facilities, we produce up to 30,000 metric tons of steel storage systems each month.
For more than two decades, our in-house engineering and R&D divisions have resolved dense space-utilization dilemmas across 120+ nations. Whether tackling high seismic ground accelerations, extreme coastal atmospheric salinity, or sub-zero logistics, our systems are calculated to international engineering standards including FEM 10.2.02, EN 15512, and Australian AS 4084 guidelines.
25+ Years of Industry Expertise proven through 10,000+ completed commercial logistics projects.
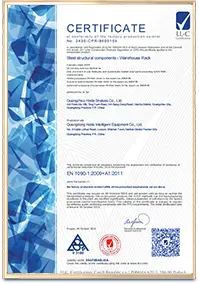
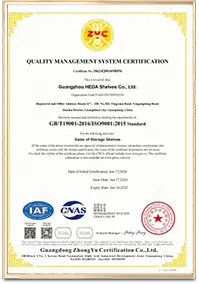
Verifiable Quality Compliance backed by CE Certificate No. 2435-CPR-8605159 and ISO 9001:2015 registration.
End-to-End Engineering Support: Complimentary CAD layout schemes, load stress analysis, and 3D visual walkthroughs.
Turnkey International Logistics: Full container-loading optimization and detailed multilingual installation blueprints.
The Future Procurement & Technological Trends in Industrial Mobile Shelving
Global supply chain disruptions, soaring commercial land costs, and energy volatility are reshaping how logistics executives source high-density storage hardware. Here are the macro shifts driving procurement today.
01
WMS-Integrated Dynamic Aisle Allocation
Modern mobile shelving systems are shifting from stand-alone manual mechanical bases to automated, API-connected architectures. Intelligent systems synchronize directly with Warehouse Management Software (WMS). When a picking order or AGV robot approaches, the appropriate aisle opens automatically, trimming travel times and cycle bottlenecks by 35%.
02
Decarbonization & Cold-Chain Energy Conservation
Refrigerated warehouse facilities represent immense continuous kilowatt-hour consumption. Because industrial mobile racking compresses cold-store structural volume by nearly 50% without reducing pallet holdings, modern procurement directors are investing in motorized mobile bases as an ESG capital asset that delivers immediate energy cost savings and rapid ROI payback.
03
Predictive Maintenance via IoT Sensor Suites
Next-generation mobile carriages integrate optical load telemetry, rail vibration sensors, and thermal drive trackers. These diagnostic modules transmit carriage health metrics directly to facility operators, warning of rail debris, uneven floor settling, or minor motor overload prior to any mechanical stoppage.
04
Hybrid Mobile Carriage & AMR Autonomous Integration
The boundary between pure racking and mobile robotics is blending. Forward-thinking procurement specifications increasingly mandate flush floor tracks designed for joint passage by Autonomous Mobile Robots (AMRs) and automated lift trucks, allowing unified goods-to-person workflows inside single-aisle mobile storage corridors.
How High-Density Mobile Shelving Solves Sector-Specific Bottlenecks
Explore how custom-tailored industrial mobile shelving configurations overcome real-world industrial constraints, from heavy tooling storage to pristine pharmaceutical cleanrooms.
Challenge: Heavy concentrated point-loads & slow crane access
Automotive Parts & Heavy Stamping Tooling
Automotive tier-1 suppliers and precision engineering plants must store hundreds of stamping dies, injection molds, and jig sets weighing up to 2,000 kg each. Conventional static shelving consumes massive plant space.
Reinforced Q235B cold-rolled steel base carriages engineered for localized shock loads
Integrated overhead crane clearance with safety interlocking anti-motion locks
Reduces mold storage floor footprint by over 60%, unlocking manufacturing floor space
Challenge: High SKU variety, mixed bin sizes, security control
Industrial Maintenance (MRO) & Hardware
Central engineering spare part depots handle thousands of fast-turnover fasteners, valves, bearings, and power tools. Mobile shelving consolidates small parts while maintaining strict visual identification.
Triple gear-ratio mechanical hand-crank assists for smooth, silent manual movement
Centralized key or digital PIN lock systems protect high-value tools from pilferage
Adjustable shelf pitches in 50 mm increments to match changing container bins
Semiconductor sub-assembly cleanrooms and national archival repositories require dust-free, non-outgassing storage setups that comply with strict fire code clearances.
RoHS-certified electrostatic conductive powder coating to dissipate static build-up
10 Factory-Controlled Steps: From Raw Steel Coil to Guided Carriages
Reliability in industrial mobile shelving depends entirely on tight manufacturing tolerances. A carriage deflection of just 2 mm can cause wheel binding. Here is how Guangzhou Heda Shelves Co., Ltd. controls every millimeter in-house.
Certified Structural Compliance for Critical Logistics Projects
Industrial mobile shelving involves dynamic moving loads and high structural weight concentrations. Safety cannot rely on unverified claims. Guangzhou Heda Shelves Co., Ltd. holds third-party audited credentials to satisfy project tenders and building inspectors worldwide:
European CE CertificationCertificate No. 2435-CPR-8605159 (Conformity with EN 15512 & EN 15095)
ISO 9001:2015 Management SystemRegistration No. 18624Q00169R0M · Design, Production & Supply Quality
RoHS Environmental DirectiveSafe, non-toxic coatings compliant for medical, pharmaceutical, and cleanroom use
Frequently Asked Questions on Industrial Mobile Shelving
Direct technical answers addressing structural calculation, civil slab requirements, sub-zero operation, and safety standards.
Need a Custom Layout Scheme?
Our senior structural engineering team provides complimentary CAD floor plans, rail foundation drawings, and dynamic load reviews tailored to your warehouse.
In static shelving or selective pallet racking layouts, fixed access aisles consume between 55% and 65% of the total warehouse floor footprint. Industrial mobile shelving mounts shelving or heavy racking columns onto motorized or mechanical wheelbases running on guided ground tracks. Because all bays pack compactly together, requiring only one "floating" picking aisle, floor space utilization jumps from ~40% to 80-90%. This effectively doubles your SKU storage capacity within the existing building envelope without requiring facility expansion.
Yes. Guangzhou Heda Shelves Co., Ltd. applies an advanced chemical pickling and phosphating pre-treatment followed by high-adhesion electrostatic thermosetting epoxy-polyester powder coating (60-80 microns). For sub-zero freezers operating down to -30°C or open coastal facilities, we supply hot-dip galvanized steel guide rails, cold-rated variable frequency drive motors, anti-condensation internal heating resistors, and cold-pliable wiring harnesses designed to prevent brittle failure.
Because mobile shelving transfers concentrated dynamic wheel loads onto steel floor rails, the warehouse concrete slab must meet stringent levelness and compressive load standards. Modern installations generally follow DIN 18202 Table 3 Group 4 guidelines (surface variations within +/- 2 mm across a 2-meter straight edge). Guangzhou Heda Shelves Co., Ltd. provides comprehensive slab loading calculations. We offer recessed grouted rail channels for new construction and surface-mounted ramped sub-floor rail kits for retrofitting onto existing finished warehouse slabs.
Our powered mobile shelving solutions are fully compliant with EN 15095 safety directives. Each carriage is equipped with floor-level photoelectric safety light curtains that immediately trigger an emergency stop if a worker, pallet, or dropped item breaks the beam. Additional safety systems include carriage-length mechanical touch-sensitive bumper bars, acoustic movement warning buzzers, flashing LED beacon towers, manual push-button emergency stops on every frame, and keyed aisle lockouts for personnel picking inside.
Power and communication commands are routed through overhead pantograph articulated cable carriers, under-floor flexible drag chains, or enclosed busbar runs. Each base carriage incorporates an independent PLC control unit and a variable frequency drive (VFD). This enables controlled soft-start and soft-stop acceleration curves that prevent stock vibration, shifting, or falling during aisle opening cycles.
To configure an accurate, safe layout, our engineering team requires: (1) Warehouse architectural drawings in CAD/PDF showing building column grids, clear ceiling height under trusses, expansion joints, and fire door locations; (2) Load specifications including weight per shelf level, box/pallet dimensions, and total expected weight per carriage; (3) Daily picking frequency and SKU throughput goals; and (4) Preferred drive system (mechanical-assist hand crank vs. automated electric PLC motor drive). We return a full 3D rendering and bill of materials free of charge within 24 hours.
"Maximize cubic space without relocating. Let us design your high-density mobile storage architecture today."
Guangzhou Heda Shelves Co., Ltd. Technical Engineering Team
Direct Factory Engineering
Request an Industrial Mobile Shelving Proposal
Send your warehouse dimensions or inventory specs. Our certified project engineers will calculate load ratings, prepare AutoCAD floor plans, and deliver a detailed commercial quote.
 Heavy Duty Automation