Featured Gravity Flow & High-Density Storage Solutions
Direct from our 30,000 m² Guangzhou manufacturing hub: precision-formed steel profiles, engineered roller tracks, and turnkey intralogistics systems calibrated for intense multi-shift fulfillment operations.
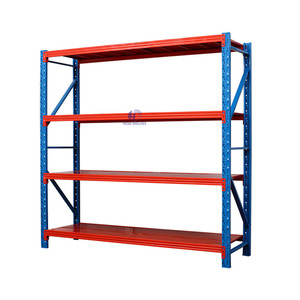
Adjustable Metal Boltless Shelf & Medium Duty Rack
Rapid boltless assembly engineered for flexible intermediate storage, kitting bins, and manual picking interfaces.
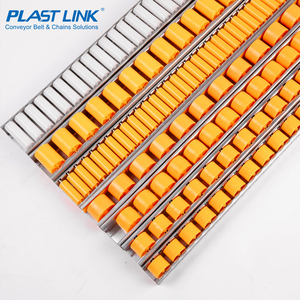
Aluminum Profile Flow Rail & Roller Track Workstation
Precision-extruded aluminum rails with high-impact polymer skate wheels and ball transfer units for lean assembly flow.
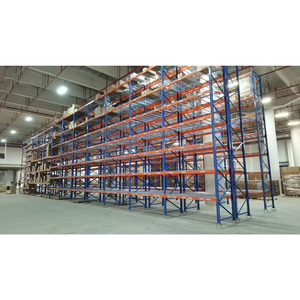
Robust Longspan Shelving Systems & Heavy Duty Shelves
High-rigidity upright design suitable for carton multi-tier setups, large case loads, and split-case picking systems.
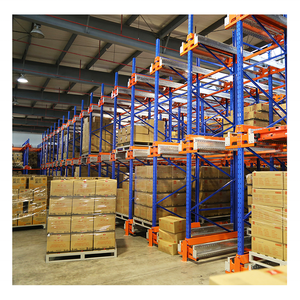
Customizable Heavy Duty Steel Pallet Radio Shuttle Rack
Dense sub-lane storage paired with automated shuttles; ideal for bulk replenishment buffers behind case picking operations.
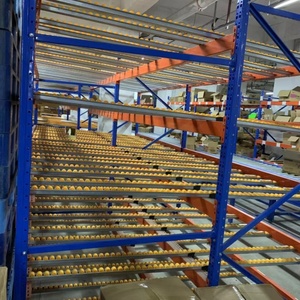
Industrial 5-Layer Heavy Duty Case Flow Gravity Rack
Ergonomic angled pick-trays and durable roller tracks guaranteeing strict First-In First-Out carton handling and picking speed.
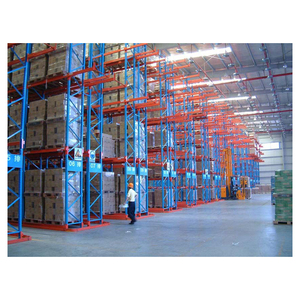
Very Narrow Aisle (VNA) Heavy Duty Racks
Engineered for high vertical clear heights and restricted aisles, maximizing building volume alongside dynamic picking decks.
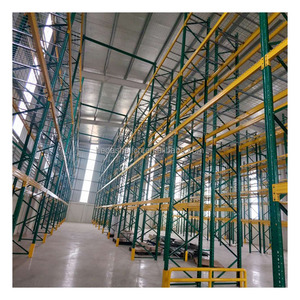
Commercial Warehouse Material Handling Racking
Heavy-duty structural upright profiles and step beams tailored for logistics centers, 3PL distributors, and packaging hubs.
Galvanized Steel Narrow Aisle Frame Racking System
Hot-dip and continuous galvanized steel structures resisting condensation, cold room thermal shocks, and aggressive chemicals.
The Physics, Geometry, and Mechanics of Industrial Case Flow Racking
In high-velocity omnichannel supply chains, SKU density and order-picking velocity dictate warehouse profitability. Case flow rack systems—frequently designated as carton flow racks, gravity flow shelving, or dynamic tote storage—represent the premier gravity-actuated intralogistics technology designed to separate stocking corridors from picking faces. As a premier China top case flow rack manufacturer & exporter, Guangzhou Heda Shelves Co., Ltd. (HEDA Shelves) engineers high-performance flow beds that harness dynamic kinetic energy to eliminate non-value-added operator travel, automate stock rotation, and protect inventory integrity.
The mechanical core of a case flow rack relies on a precisely calibrated decline angle, typically specified between 2.5 degrees and 4.5 degrees (equivalent to a 4.5% to 8% pitch), dependent upon packaging friction coefficients, total carton weight, and roller bed bearings. Under continuous gravitational force, totes, corrugated cases, or plastic bins glide from the rear loading interface to the front discharge apron. As front items are retrieved, trailing cartons glide forward automatically. This creates an uncompromised First-In, First-Out (FIFO) stock control cycle, an operational prerequisite for food and beverage, pharmaceuticals, cold-chain distribution, and automotive assembly operations.
Gravitational Incline Control
Engineered drop-in pitch adjusters allow multi-level slope tuning from 2° to 5°. Ensures consistent glide velocities without uncontrolled runaway speeds or carton jamming.
High-Impact Roller Physics
Precision-molded virgin polypropylene (PP) or ultra-high-molecular-weight polyethylene (UHMW-PE) wheels fitted with zinc-plated steel axles and low-friction bearings for long lifecycle endurance.
Ergonomic Tray Integration
Cantilevered presentation shelves tilt picking cartons 15° to 25° toward the operator. Dramatically reduces lumbar strain, minimizes repetitive motion fatigue, and boosts lines-per-hour speed.
Modern case flow racks are categorized by their wheel beds: Track-based roller systems utilize discrete lanes of plastic or steel wheels dedicated to specific SKU widths, while Full-width roller deck beds (or universal dynamic beds) deploy continuous roller arrays allowing unlimited carton width flexibility without repositioning physical track guides. Structural framework profiles supplied by HEDA Shelves utilize high-yield Q235B and Q355B structural steel, cold-formed into omega-profile upright columns and heavy-duty box step beams conforming to international standards (EN 15512, RMI, and ISO 9001:2015).
Future Sourcing & Procurement Trends: Case Flow Systems (2025–2030)
Procurement leaders, supply chain vice presidents, and 3PL infrastructure planners must account for massive shifts in omnichannel consumer habits, micro-fulfillment node proliferation, and warehouse automation integration. Sourcing case flow solutions from China has evolved beyond simple structural fabrication to procuring complete, precision-toleranced intralogistics components ready for hybrid human-robotic picking cells.
1. Cobot & AMR Picking Coexistence
Future case flow racks must provide high-precision shelf stops and laser-calibrated end stops to allow vision-guided Autonomous Mobile Robots (AMRs) and robotic arms to pick directly from gravity-presented cartons without misalignment.
2. Micro-Fulfillment Modularization
Urban distribution centers require boltless, highly modular flow frames that warehouse operators can reconfigure overnight. Tool-less clip-in roller assemblies and snap-fit track dividers allow immediate adaptation to rapid seasonal SKU shifts.
3. Sub-Zero Cold Chain Polymers
Rapid expansion in fresh food grocery fulfillment has triggered surging demand for specialized polyoxymethylene (POM) and anti-static roller compounds engineered to eliminate brittle-fracture failure under deep freezing at -30°C.
| Procurement Metric | Traditional Static Shelving | Standard Carton Flow | HEDA Engineered Heavy Case Flow |
|---|---|---|---|
| Pick Face Density (SKU/m²) | Low (Aisles required on both sides) | Moderate (Dedicated feed/pick faces) | Maximum (Up to 300% denser storage footprint) |
| Operator Travel Reduction | 0% (Standard walking route) | 50% - 60% Reduction | Up to 75% Compression of picker paths |
| Stock Rotation Reliability | Poor (Operator-dependent LIFO risk) | High (Strict Gravity FIFO) | Absolute FIFO + Dynamic Speed-Regulators |
| Pick-to-Light / RFID Ready | Difficult & Dispersed | Compatible | Pre-Engineered Mounting Channels integrated |
| Long-Term Lifecycle TCO | High labor cost overhead | Moderate Capex, Low Opex | Lowest Total Cost of Ownership (Fast 6-12 Mo ROI) |
Why Global Supply Chains Partner with HEDA Shelves
Headquartered in Guangzhou, China, Guangzhou Heda Shelves Co., Ltd. has led the commercial warehousing and industrial racking sector since 2001. Operating a modernized 30,000 square meter factory backed by a 300+ strong workforce of licensed structural engineers, CAD draftspersons, and certified welders, HEDA Shelves delivers over 30,000 metric tons of steel storage systems every month to clients spanning over 120 countries across Southeast Asia, North America, Europe, Australia, and the Middle East.
Our international export dominance is founded upon complete vertical integration. Unlike assemblers who outsource critical components, HEDA manufactures upright frames, step beams, roller assemblies, guide dividers, and brackets under one roof. Our facilities carry CE Certification (No. 2435-CPR-8605159), ISO 9001:2015 Quality Management (No. 18624Q00169R0M), and RoHS Compliance, verifying material traceabilities and structural calculations under heavy dynamic load conditions.
10-Stage In-House Precision Manufacturing Methodology
Every case flow component follows strict dimensional tolerance protocols, ensuring smooth field assembly and zero friction for dynamic rollers:
Raw Material
Certified prime Q235B/Q355B coiled steel with certified tensile properties.
CNC Slitting
Laser and high-speed rotary shearing with sub-millimeter tolerances.
Automated Punching
Continuous hydraulic stamping of pitch holes (50mm/75mm intervals).
Roll Forming
Multi-stand cold rolling creating rigid omega and step beam profiles.
Robotic Welding
Shielded arc welding of heavy beam connectors and end flanges.
Polishing & Deburr
Automated grit blasting removing spatter and surface mill scale.
Pickling & Phosphate
Multi-stage chemical degreasing for tropical anti-corrosion bonding.
Powder Coating
Automated electrostatic spray with durable 60-80 micron epoxy finish.
Thermal Curing
200°C oven curing ensuring scratch, chip, and humidity resistance.
QC & Bundling
Container-optimized bundle strapping with barcode export labeling.
Frequently Asked Questions by International Buyers
Direct engineering answers regarding structural capacities, incline angles, maintenance protocols, and shipping logistics from China.
Transform Your Order Picking Productivity Today
Contact HEDA Shelves' technical sales engineering team to receive customized CAD layouts, structural load calculations, and competitive factory-direct pricing for your next warehouse storage upgrade.