Featured Industrial Racking & High-Density Mobile Platforms
Engineered in our 30,000 m² ISO 9001:2015 and CE-certified production center. These 8 flagship systems represent precision cold-rolled profile forming, custom load distribution, and multi-tier space efficiency designed for cross-border logistics reliability.
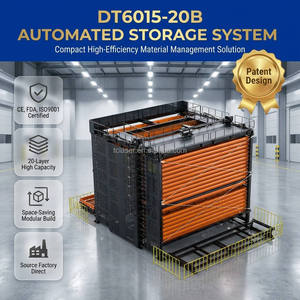
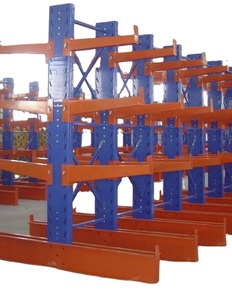
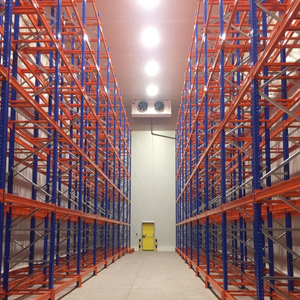
Engineering Analysis: Procuring High-Density Industrial Mobile Shelving Systems from China
In modern industrial supply chains, floor space is an escalating operational expenditure. Conventional static racking configurations dedicate upwards of 55% to 65% of warehouse floor footprint strictly to operating aisles. As land acquisition costs in primary logistics hubs (such as Singapore, Port Klang, Bangkok, Manila, Jakarta, Rotterdam, and Los Angeles) surge, international operations executives increasingly look to specialized Chinese manufacturing centers for heavy-duty electric and mechanical-assist mobile shelving systems.
A mobile shelving system (also known as a mobile compactor or mobile pallet racking system) mounts structural racking bays onto heavy-duty motorized or geared wheel bases that travel across precision-embedded floor rails. By eliminating redundant static access aisles, a mobile shelving cluster condenses an entire warehouse block into a single dynamically opened corridor. This engineering achievement boosts volumetric storage density by 80% to 100% while retaining 100% direct selectivity to any SKU when prompted via warehouse control software (WCS) or manual command.
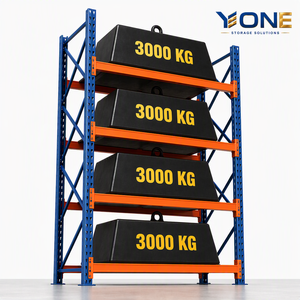
Critical Engineering Principle: True space optimization must never compromise structural safety margins. Mobile shelving bases carry dynamic live loads exceeding 24 tons per carriage. As an industry leader established in 2001, Guangzhou Heda Shelves Co., Ltd. builds structural frameworks that calculate seismic acceleration, wheel-to-rail friction coefficients, and steel yield fatigue under FEM 10.2.02 and EN 15512 standards.
Enterprise Advantages: Why HEDA Shelves Sets the Benchmark for Chinese Exporters
Selecting an export partner for complex intralogistics machinery requires a stringent evaluation of manufacturing provenance, metallurgical traceability, and engineering design depth. Operating directly from our 30,000 m² heavy-manufacturing infrastructure in Guangzhou, China, HEDA Shelves has served as a specialized engineering backbone for global third-party logistics (3PLs), multinational pharmaceutical cold chains, automotive assembly plants, and government archival facilities for over two decades.
Unlike trading entities or regional assembly shops, our factory integrates every phase of fabrication under an accredited ISO 9001:2015 Quality Management framework (Certificate No. 18624Q00169R0M) and rigorous European CE Conformity standards (CE Marking No. 2435-CPR-8605159):
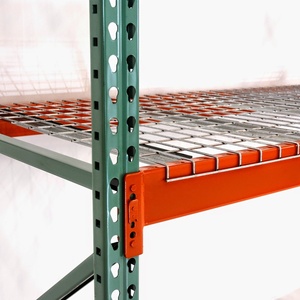
1. Structural Steel Formulation & Profile Integrity: We utilize certified prime Q235B and high-yield Q355B cold-rolled structural steel coils sourced directly from top-tier domestic mills. Our automated multi-station cold roll-forming lines shape continuous upright profiles with optimized inertia moments, ensuring that our mobile carriages resist lateral torsional buckling even during abrupt emergency stops or maximum-load rail transits.
2. Advanced Tropicalized Pre-Treatment & Surface Finishing: Cross-border shipments headed to Southeast Asia, Oceania, the Middle East, or Latin America encounter hyper-saline maritime air and ambient relative humidity exceeding 85%. While substandard manufacturers coat directly over lightly wiped steel, HEDA enforces a comprehensive 10-stage preparation sequence: precision automated cutting, continuous CNC column punching, multi-head robotic welding, immersion degreasing, industrial pickling, phosphating passivation, and electrostatic powder coating baked at 200°C. For deep-freeze cold stores (-30°C) and corrosive chemical yards, heavy-duty hot-dip galvanization is executed to eliminate premature rust pitting.
3. Comprehensive In-House Engineering & Free 3D/CAD Layouts: Before any steel coil is unrolled, our engineering bureau of over 300 technical and manufacturing professionals generates complete structural calculations, aisle clearance simulations, wheel-load distribution charts, and DWG/BIM drawings. Global buyers receive clear structural documentation ready for submission to local building inspectors and insurance underwriters.
| Storage Architecture | Footprint Utilization | Selectivity | Initial Capex | Energy & Climate Control ROI |
|---|---|---|---|---|
| HEDA Heavy-Duty Mobile Shelving | 85% – 90% (Maximum) | 100% Direct SKU Access | Moderate – High | Highest (Cuts refrigerated volume by up to 50%) |
| Selective Pallet Racking | 35% – 45% (Aisle Intensive) | 100% Direct SKU Access | Low | Low (Heats/cools wasted aisle air) |
| Drive-In / Drive-Through Rack | 70% – 75% (Dense) | Poor (Strict LIFO / FIFO batch) | Moderate | Moderate (Risk of internal forklift impact) |
| Automated AS/RS Crane System | 90% – 95% (Vertical Max) | 100% Automated Access | Extremely High | High (Substantial power & maintenance footprint) |
Future Procurement & Technological Trends in Mobile Shelving (2025–2035)
Procurement teams are shifting away from evaluating storage strictly as static steel hardware. Industrial mobile shelving systems have matured into intelligent, sensor-driven electromechanical assets. International buyers specifying mobile compactors must anticipate three core market trends shaping global warehouse operations:
1. Industry 4.0 & WMS/WCS Autonomous Mobilization: The modern mobile shelving system no longer relies solely on manual operator keypads. Leading automated distribution hubs interface mobile bases directly with corporate ERP and Warehouse Management Systems via industrial wireless protocols (Profinet, EtherCAT, or industrial Wi-Fi). When an incoming picking batch or autonomous mobile robot (AMR) is routed to an aisle, the mobile compactor automatically moves along its rails in advance, presenting an open aisle just as the equipment arrives. This intelligent pre-positioning eliminates operator wait times and multiplies pick rates.
2. Optical Multi-Zone Safety Curtains and Redundant Sensor Grids: Workplace safety mandates in Europe (EN 15095) and North America (OSHA/ANSI standards) require absolute operator protection within moving aisle corridors. Contemporary mobile shelving features continuous photoelectric safety beams spanning the bottom toe level, mid-carriage height, and top-tier overheads. If a worker, a stray carton, or a pallet overhang interrupts the optical curtain while a carriage is in motion, electronic zero-backlash braking circuits instantly halt all motors within 100 milliseconds.
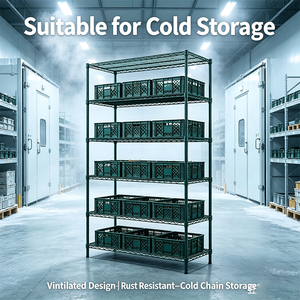
3. Cold-Chain Condensation Control & Night-Parking Energy Modes: Driven by explosive growth in biologics, cold-chain pharmaceuticals, and frozen food logistics across ASEAN and global supply corridors, mobile shelving is increasingly specified for sub-zero freezer chambers (-25°C to -30°C). Because cooling unoccupied open aisles wastes electrical energy, modern smart mobile systems feature an automated "Night Parking Mode." At the close of operations, carriages automatically separate by an equal distance of 150–200 mm across the entire room, facilitating balanced cold-air circulation, preventing moisture condensation pockets, and reducing chiller refrigeration loads by up to 45%.
Dual-Flange Steel Wheels
Forged C45 alloy steel wheels heat-treated to HRC 45-50, running on precision milled rails to prevent carriage skew and ensure zero-vibration motion.
Variable Frequency Drives
Soft-start and soft-stop acceleration curves controlled via integrated VFD units prevent shifting, tipping, or jarring of stacked industrial goods.
Seismic Interlock Hooks
Engineered anti-topple anchor rails and high-tensile bottom mechanical latches safeguard multi-tier carriages in active seismic zones.
Modular Rail Embedding
Direct floor leveling systems support both embedded flush installation (for smooth forklift crossings) and surface ramping configurations.
Frequently Asked Questions: Sourcing Mobile Shelving from China
Detailed engineering, logistical, and commercial answers for international procurement managers and project consultants.
Q1: How does HEDA ensure floor rail precision when exporting to overseas warehouse facilities?
Mobile shelving systems require strict floor flatness and rail level tolerances (typically within ±1.5 mm over a 10-meter span). HEDA provides specialized heavy-duty leveling bolts, ground rail shims, and high-tensile chemical anchors with every export package. Furthermore, our engineering bureau supplies step-by-step CAD rail foundation drawings, detailing floor trench depth, secondary non-shrink grouting procedures, and rebar bonding requirements to ensure local concrete contractors achieve flawless alignment.
Q2: Can your mobile shelving electrical systems accommodate different international voltage standards?
Yes. Every electric mobile compactor drive panel and motor grouping is customized in-factory to match the destination country's three-phase grid specifications—including 380V/50Hz (ASEAN, Europe, China), 415V/50Hz (Malaysia, UK, Australia), 480V/60Hz (USA), or 220V/60Hz (Philippines, South Korea). All internal switchgear, contactors, and programmable logic controllers (PLCs) utilize globally recognized components from Schneider Electric, Siemens, or Omron, ensuring long-term parts availability worldwide.
Q3: What are the typical sea transit durations from Guangzhou port to major export hubs?
Situated in Guangzhou near the major container terminals of Nansha, Huangpu, and Shenzhen, HEDA Shelves offers fast vessel departures. Estimated ocean transit to Southeast Asian gateways includes: 2–5 days to Vietnam (Haiphong/Cat Lai), 3–5 days to the Philippines (Manila), 5–7 days to Singapore and Thailand (Laem Chabang), 6–8 days to Malaysia (Port Klang), and 7–10 days to Indonesia (Jakarta). For European, Middle Eastern, and American destinations, direct vessel lines ensure dependable shipping under both FOB and CIF terms.
Q4: How does HEDA protect precision mechanical carriages from ocean container moisture and corrosion?
Cross-ocean transit subjects steel cargo to high temperature swings and enclosed maritime condensation. Beyond our 10-stage pickling, phosphating, and powder-coating treatment, all exposed wheel bearings, drive shafts, and transmission gear teeth receive industrial-grade anti-rust protective wax. Components are systematically wrapped in vapor-barrier polythene sheeting, bundled on steel runners with corrugated cushioning, and secured within 40HQ containers using cross-braced ratchet banding to prevent transit shifting.
Q5: What documentation is provided to satisfy local building codes and seismic regulations?
Every structural proposal includes comprehensive engineering dossiers: 2D architectural CAD layouts, 3D volumetric schematics, upright and beam cross-sectional inertia properties, dynamic wheel-load calculations, and structural calculation reports compliant with CE No. 2435-CPR-8605159. For active seismic regions such as Indonesia, Japan, New Zealand, or the Philippines, our engineering team integrates localized seismic spectral coefficients into structural bracing and floor anchoring designs.
Q6: What is the operational lifespan and maintenance protocol for a heavy-duty electric mobile system?
HEDA mobile shelving structural steel carries a designed operational service life exceeding 20 years under rated load limits. Mechanical components (dual-flange wheels, precision gearboxes, drive chains) are engineered for heavy cyclic durability. Maintenance simply involves semi-annual lubrication of drive chains and bearings, optical sensor lens cleaning, and inspection of rail sweep brushes that keep floor tracks clear of loose debris.