Heavy Duty
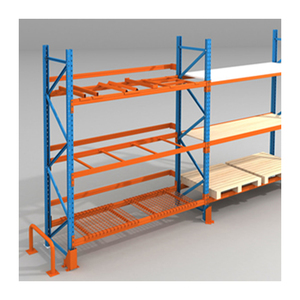
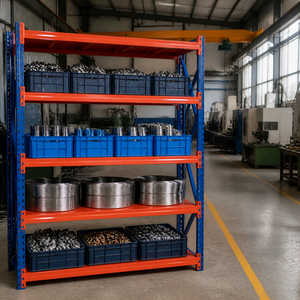
Dual-Purpose Industrial Warehouse Racking System 5-Layer Storage Rack
- Q235B / Q355B Steel
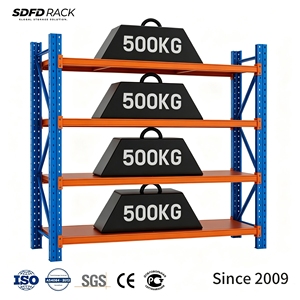
- 1,000–4,500 kg/Beam
- Corrosion Resistant
Engineered to comply with stringent European standard EN 15512 and FEM 10.2.02 codes. Each configuration undergoes precision finite element structural analysis, automated roll forming, and 10-stage pre-treatment coating.
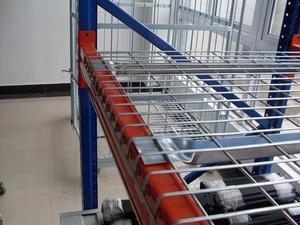
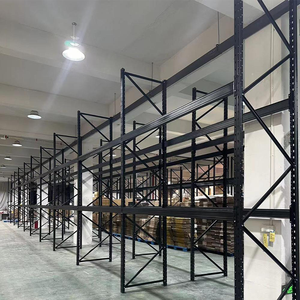
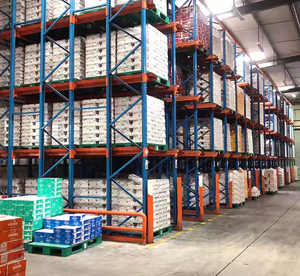
Pallet racking in high-throughput distribution centers is not mere industrial furniture; it is load-bearing structural equipment governed by international building codes. Procuring from CE-certified factories protects your capital asset from catastrophic buckling, racking collapse, and costly civil liabilities.
Under the Construction Products Regulation, racking structural steel must meet harmonized standard EN 15512:2020. This standard dictates second-order p-delta global stability calculation, beam-end connector moment-rotation stiffness ($C_d$) test verification, and minimum safety factors against column flexural-torsional buckling under ultimate limit states (ULS).
Certified supply factories source primary mill-certified structural coil (Baosteel / Shougang) rather than non-certified rerolled billets. High-yield Q355B ($f_y \ge 355 \text{ MPa}$) is calibrated for upright sections to resist heavy seismic lateral forces, while carbon-controlled Q235B ($f_y \ge 235 \text{ MPa}$) provides maximum ductility in cold-formed box beams.
EN 15620 dictates serviceability limit state (SLS) beam deflection must never exceed $\delta \le L/200$ for standard pallet configurations, and $\delta \le L/300$ for automated crane and VNA turret truck operations. Rigorous factory test rigs verify that residual permanent deflection stays below $0.15\%$ after $125\%$ load release.
| Evaluation Parameter | CE-Certified HEDA Industrial Racks | Low-Cost Non-Certified Rack Suppliers | Operational Consequence & ROI Impact |
|---|---|---|---|
| Certification & Factory Audit | CE (2435-CPR-8605159) & ISO 9001 | None / Self-Declared Declaration | Complies with local municipal and insurance fire/safety inspections. Eliminates shutdown orders. |
| Cold-Formed Steel Grade | Prime Q235B & Q355B with mill-test chemistry certificates (MTC) | Mixed secondary coils, high sulfur & phosphorus, variable thickness | Guaranteed yield stress preventing sudden catastrophic bracket shear under peak design loads. |
| Surface Pretreatment | 10-step immersion pickling, degreasing, phosphating, and deionized rinse | Wipe-down or single-stage solvent spray before paint | Superior powder coating adhesion; exceeds 500-hr salt-spray corrosion tests in tropical or humid environments. |
| Beam-to-Column Connector | Precision 3/4/5-prong teardrop / diamond cold-stamped claws with safety pins | Hand-welded 2-prong flat tabs with loose bolts | High rotational rigidity ($C_d$); prevents accidental beam dislodgement caused by forklift impact. |
| Seismic Structural Design | Engineered per localized Eurocode 8 / ASCE 7 ground acceleration | Uniform unengineered configuration regardless of seismic zone | Reinforced baseplates, oversized chemical anchors, and cross-bracing eliminate sway failure in fault lines. |
Global supply chain turbulence, rising industrial real estate costs, and strict ESG compliance are redefining how global buyers evaluate pallet rack suppliers. Forward-thinking operations align capital expenditure with these four distinct engineering shifts.
Procurement is moving rapidly away from low-density wide-aisle configurations toward semi-automated 4-way radio shuttle systems and AS/RS interfaces. Buyers require racking manufacturers capable of producing high-precision rails with cumulative tolerances under $\pm 1.5 \text{ mm}$ over 60 meters to prevent shuttle vehicle derailments.
With global pharmaceutical and frozen food cold chains scaling rapidly, procurement managers are specifying dual-layer finishes: hot-dip galvanizing (EN ISO 1461, minimum 65 $\mu m$ zinc thickness) or zinc-rich electro-epoxy priming under heavy polyester topcoats to prevent micro-corrosion in continuous $-30^\circ\text{C}$ condensation cycles.
Modern tier-1 logistics operators demand CAD files pre-formatted for BIM (Building Information Modeling) and Digital Twin asset trackers. Factories that provide native IFC and Revit families with integrated load capacity tables allow structural engineers to run real-time telemetry simulations before pouring building slab footings.
Corporate sustainability mandates require lower embodied carbon in warehouse construction. Supply factories that utilize ultra-high-strength thin-walled profiles (minimizing structural steel tonnage while maintaining EN 15512 safety factors) and non-toxic, TGIC-free powder formulations lead global enterprise vendor selections.
The technological horizon of industrial storage lies in precision micro-geometry. Guangzhou Heda Shelves pioneers the integration of advanced cold-work hardening profiles that elevate structural performance without adding unnecessary dead weight.
Upright columns engineered with 11 to 13 continuous cold-rolled bends (the Omega-Fold geometry) distribute axial stress along multiple longitudinal ribs. This structural cross-section drastically suppresses torsional-flexural buckling compared to conventional 5-fold C-channels, enabling upright heights exceeding 18 meters.
Modern heavy-duty load beams utilize robotic continuous CO2 gas-shielded welding joining two cold-rolled 'C' sections face-to-face. This creates a closed rectangular tubular beam with a superior section modulus ($W_x$) and polar moment of inertia, eliminating the lateral torsional twisting typical of open step beams.
In seismic risk areas such as the Pacific Rim and Mediterranean zones, rigid anchoring can cause catastrophic floor slab shear. HEDA supplies engineered energy-dissipative baseplate assemblies with slotted anchoring and calibrated yield washers that absorb horizontal acceleration impulses without failing.
With over 25 years of engineering leadership, our 30,000 square meter facility in Guangzhou manufactures over 30,000 tons of structural steel racking every month. Every component is produced under strict ISO 9001:2015 and CE certification protocols across a dedicated 10-stage fabrication line.
Spectrographic verification of prime Q235B/Q355B coils for yield strength and elongation.
Automated uncoiling and laser-guided slitting within $\pm 0.1 \text{ mm}$ width tolerance.
Heavy tonnage high-speed mechanical press punching pitch holes (50mm/75mm) in single passes.
Continuous 16-stand roll-forming line gradually forming closed, multi-ribbed upright sections.
Cold-forming opposing C-profiles engineered for automatic nesting and seam preparation.
Dual-station 6-axis welding robots fusing connector claws with continuous spatter-free beads.
Alkaline chemical immersion eliminating residual rolling oils and drawing compounds.
Acid immersion descaling followed by zinc-phosphate chemical bonding conversion layer.
Nordson automated powder guns applying 80–120 $\mu m$ pure polyester cured at 200°C.
Cross-hatch adhesion, ultrasonic thickness testing, and heavy-gauge export wood buffering.
Receive comprehensive structural proposals, 3D renderings, and warehouse floor optimization layouts within 24 to 48 hours—fully verified by our in-house structural engineers.
Positioned near Guangzhou and Nansha international ports, sea transit is exceptionally rapid: 2–5 days to Vietnam, 3–5 days to Manila, 5–7 days to Singapore, and 6–8 days to Port Klang.
Precision component nesting and heavy-duty steel framing maximize 40HQ container cube volume to 99.2%, reducing international shipping cost per pallet position by up to 28%.
Definitive engineering answers for international project managers, logistics directors, safety consultants, and procurement executives evaluating factory-direct racking orders.
Maximize your facility's cubic pallet capacity while guaranteeing structural safety compliance under CE & EN 15512. Connect directly with our senior racking engineering specialists in Guangzhou for free CAD layout optimizations, structural load calculations, and factory-direct volume pricing.