High-Throughput Warehouse Roller Racks & Dynamic Flow Racks
Explore our export-certified roller rack configurations engineered for precision SKU order picking, high-density live pallet accumulation, mold accessibility, and rapid logistics order fulfillment.
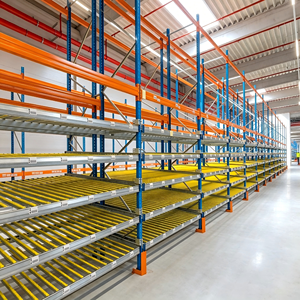
Gravity Carton Flow Racking Adjustable Roller Carton Flow Shelving FIFO
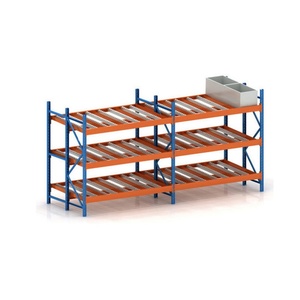
Steel Automated Retrieval Flowing Type Sliding Rolling Rack System
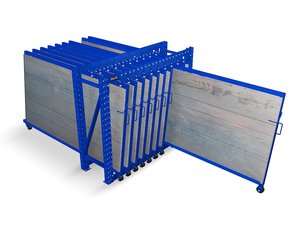
Vertical Roll Out Sheets Rack Drawer Storage Rack for Sheet Metal
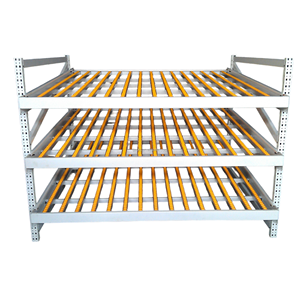
Collapsible Powder-Coated Logistics Mobile Gravity Pallet Roller Rack
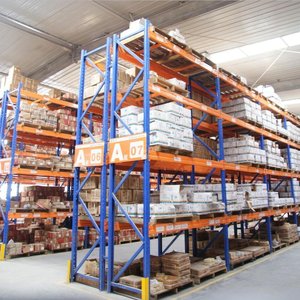
Heavy Duty Steel Mold Storage Rolling Drawer Racks Shelving Unit
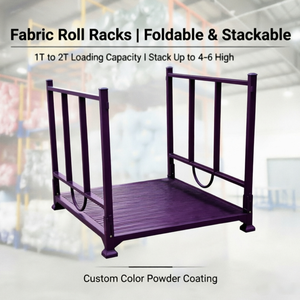
Mobile Fabric Roll Storage Rack Foldable Stackable Rolling Steel Rack
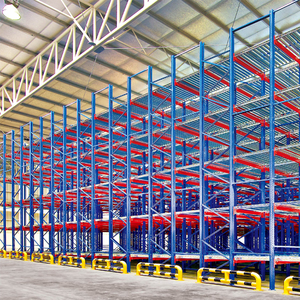
Adjustable High Space Utilization Warehouse Gravity Flow Roller Shelving
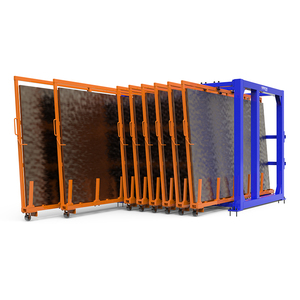
Multi-Tier Adjustable Foldable Vertical Roll-Out Rack System with Wheels
Why International Industrial Buyers Partner with HEDA Shelves
Headquartered in Guangzhou since 2001, Guangzhou Heda Shelves Co., Ltd. operates a premier 30,000 m² automated production facility exporting heavy-duty dynamic racking, structural mezzanines, and precision gravity flow storage solutions to over 120 nations worldwide.
In modern industrial logistics and omnichannel supply chain operations, storage systems cannot be viewed as static structural steel assemblies. Modern distribution centers face aggressive SKU multiplication, volatile picking demands, and stringent safety regulations. As one of the world's most trusted warehouse roller racks suppliers and exporters, HEDA Shelves provides full-lifecycle engineering support: from precision computer-aided structural layout design (AutoCAD, Autodesk Revit 3D) and dynamic finite element analysis (FEA) to high-precision cold roll-forming, automated CNC multi-station hole punching, and automated electrostatic powder coating.
Our gravity flow roller racks are designed strictly in accordance with EN 15512, EN 15620, RMI (Rack Manufacturers Institute), and AS 4084 standards. Backed by verified CE Certification (No. 2435-CPR-8605159), ISO 9001:2015 Quality Management (No. 18624Q00169R0M), and complete RoHS environmental compliance, our systems guarantee deterministic dynamic carton and pallet velocity, long-term fatigue resistance, and fail-safe seismic performance.
25+ Years Racking Engineering
Over two decades of dedicated research into material properties, cold roll profile optimization, gravity friction mechanics, and structural steel dynamic behavior under intensive loading cycles.
- 300+ professional technical staff
- Bespoke custom OEM & ODM engineering
Free 3D & CAD Layout Service
Our senior intralogistics architects provide complimentary 2D floor plans, 3D parametric renderings, aisle optimization studies, and load deflection calculations prior to contract finalization.
- Turnaround within 24 to 48 hours
- Optimized for forklift & AMR clearances
Tropical Anticorrosion Protection
All structural steel components undergo a proprietary 9-stage degreasing, acid pickling, and phosphating pre-treatment before receiving automated electrostatic thermoset powder coating.
- Resists 85%+ relative humidity
- Hot-dip galvanized options for cold chains
Global Export & Fast Transit
Located near major ocean hubs in Guangzhou and Nansha, we provide container-optimized nesting and crating, delivering direct to port with indicative transit times as fast as 2 to 10 days across Asia.
- FOB, CIF, CFR, DDU/DDP terms
- Installation drawings & video supervision
The Physics of Gravity Roller Racks: Critical Design Parameters
A comprehensive technical evaluation of slope angles, roller wheel types, braking mechanics, and structural deflection formulas for system integrators and procurement directors.
Gravity roller racks operate on an elegant zero-energy dynamic principle: transforming gravitational potential energy into controlled linear kinetic movement. However, achieving smooth, safe carton or pallet transit requires precise balancing of the static friction coefficient ($\mu_s$), rolling resistance ($\mu_r$), and kinetic acceleration ($a = g \cdot (\sin\theta - \mu \cdot \cos\theta)$).
If the track pitch is insufficient, lightweight totes and corrugated cartons will stall mid-lane, forcing operators to push goods manually and destroying picking ergonomics. Conversely, excessive pitch produces hazardous terminal velocities, causing high-impact collisions at the pick face, damaged packaging, or dislodged inventory.
HEDA Engineering Guideline: Slope Gradient Matrix
Standard carton flow systems require a calibrated pitch of 2.5° to 3.5° (approx. 4.5% to 6% slope) for uniform plastic bins and rigid paper cartons. Heavy-duty pallet flow systems utilizing wooden Euro pallets or GMA pallets require 1.5° to 2.5° (approx. 3% to 4.5% slope) combined with speed controller braking rollers spaced every pallet position.
| System Type | Track & Roller Composition | Max Load per Unit | Ideal Incline Angle | Speed Control Mechanism | Primary Application |
|---|---|---|---|---|---|
| Carton Flow Racking | High-density polyethylene (HDPE) skate wheels or aluminum fluent strips | 30 kg – 100 kg / Carton | 2.5° – 3.5° | Passive friction dividers & cushioned end stops | E-commerce fulfillment, pick-to-light picking lines, pharmaceuticals |
| Heavy Pallet Flow Racks | Zinc-plated high-grade steel cylindrical rollers with sealed bearings | 500 kg – 1,500 kg / Pallet | 1.8° – 2.5° | Centrifugal dynamic brake rollers & safety pallet separators | Cold storage staging, beverage distribution, date-critical FIFO bulk stock |
| Vertical Roll-Out Sheet Rack | Telescopic steel guides with hardened dual-flanged guide wheels | 1,000 kg – 3,000 kg / Level | 0° (Horizontal mechanical pull-out) | Mechanical crank / lockable manual slide arrestors | Sheet metal fabrication, CNC laser cut feeding, heavy raw material staging |
| Mold Storage Drawer Rack | Machined solid steel roller bearings with dual-rail sliding guides | 1,000 kg – 2,500 kg / Shelf | 0° (Precision horizontal extension) | Multi-point mechanical drawer lock & anti-tip interlocking bar | Injection mold shops, stamping tool rooms, die-casting tool libraries |
| Mobile Fabric Roll Rack | Polyurethane cast iron casters + heavy steel cradle bars | 500 kg – 1,200 kg / Rack | Flexible roll staging | Total-lock foot brakes & floor guidance rail grooves | Textile manufacturing, carpet warehousing, film and vinyl converter hubs |
Structural Deflection and Steel Tolerances: In heavy gravity roller lanes, the beam deflection ratio under full design load must not exceed $L/250$ (where $L$ is clear beam span length), as structural sag causes roller axis deviation, introducing severe lateral skew that can jam cartons against side guides. HEDA uprights are engineered from premium grade Q235B or Q355B high-tensile cold-rolled steel coils with continuous roll-formed profile sections for maximum structural rigidity and exceptional impact energy absorption.
10 Controlled Stages from Steel Coil to Export Container
By producing every upright column, dynamic roller bed, fluent strip frame, and safety accessory completely in-house, HEDA Shelves eliminates third-party subcontractor variance and ensures absolute batch consistency.
Raw Steel Inspection
Certified steel coil verification for yield tensile strength and chemical purity.
Precision Slitting
Automated uncoiling and high-speed longitudinal slitting to strict tolerances.
CNC Column Punching
Continuous CNC multi-station hole punching ensuring pitch precision within 0.1 mm.
Cold Roll-Forming
18-station cold roll profile forming for high section modulus and load rigidity.
Profile Calibration
Automated flying hydraulic cut-off and laser dimensional verification.
Robotic Welding
MIG/CO2 robotic beam and connector bracket welding for seamless weld beads.
Surface Polishing
Mechanical blast cleaning and slag removal to eliminate burrs and sharp edges.
Pickling & Phosphating
9-stage chemical immersion bath creating an optimal anti-corrosive passivation layer.
Powder Coating
Automated electrostatic epoxy powder coating cured in a 200°C continuous tunnel kiln.
Pre-Shipment QA
Load testing, coating thickness check, container nesting, and bundle crating.
Emerging Procurement Trends Shaping Gravity Roller Storage
Key technological shifts and procurement criteria influencing warehouse management, automation compatibility, and capital expenditure decisions over the next decade.
Integration with Autonomous Mobile Robots
Modern fulfillment operations are transforming gravity roller racks into high-throughput hand-off buffers for autonomous mobile robots (AMRs). Roller tracks equipped with pneumatic release latches and optical sensors allow AMRs to drop totes at the replenishment face and retrieve picked cartons at the discharge face without human intervention, creating a low-cost, hybrid automated picking cell.
Modular Track Reconfiguration & Fast-Slotting
With seasonal e-commerce fluctuations and shifting carton dimensions, fixed-width gravity lanes are being rapidly replaced by modular, tool-free adjustable fluent strip beds. Procurement teams prioritize clip-in plastic skate wheel tracks that allow warehouse floor supervisors to reconfigure lane widths, add intermediate dividers, and adjust shelf inclinations in minutes without disassembling primary structural beams.
Pick-to-Light (PTL) & RFID Telemetry
Intelligent roller racks are increasingly fitted with integrated digital bus lines for Pick-to-Light (PTL) LED modules, digital quantity displays, and micro-switch load sensors. When an operator pulls a carton from the roller pick face, the next carton rolls forward, tripping a gravity sensor that automatically updates the WMS (Warehouse Management System) inventory level in real time, virtually eliminating pick discrepancies.
Sub-Zero Condensation & Cryogenic Resilience
Rapid expansion in frozen food and biopharmaceutical distribution demands gravity roller systems capable of operating non-stop at temperatures as low as -30°C. Buyers are shifting toward specialized low-temperature synthetic lubricants inside roller bearings, composite impact nylon wheels that resist thermal embrittlement, and hot-dip galvanized steel frames that prevent galvanic corrosion caused by defrost cycling.
Total Cost of Ownership (TCO) Prioritization
Procurement directors are calculating 10-year Total Cost of Ownership rather than simply comparing initial steel tender pricing. Key cost drivers include roller bearing sealing quality, roller wall thickness (1.5 mm vs. 1.0 mm), powder coat impact chipping resistance, and spare parts availability. Sourcing factory-direct from vertically integrated manufacturers like HEDA ensures long-term track component backward-compatibility.
Pacific Rim & Seismic Zone Engineering
With massive logistics growth across seismic zones in Southeast Asia, Japan, and the Americas, buyers require structural load calculations that factor in seismic drift, baseplate anchor shear stresses, and rack dynamic response under horizontal ground acceleration, requiring heavy-duty box-beam upright bracings and high-ductility base connections certified by independent structural engineers.
Global Supply Chain Delivery: Direct from Guangzhou
Strategically situated near the major international shipping hubs of Guangzhou and Nansha, HEDA Shelves provides frictionless export crating, customs documentation, and expedited maritime container shipping.
A successful cross-border racking procurement project depends heavily on logistics execution. Structural steel and roller components are vulnerable to transit damage, sea moisture exposure, and shipping container volumetric inefficiencies if packed improperly. At HEDA Shelves, all upright frames, beams, and fluent roller beds are systematically grouped by erection sequence, interleaved with shock-absorbing foam membranes, corner-protected with heavy corrugated steel angle guards, and steel-banded onto custom heavy-duty export skids.
Our dedicated container loading engineers calculate three-dimensional container packing plans (using advanced container nesting software), guaranteeing maximum cubic utilization across 20GP, 40GP, and 40HQ ocean containers. This directly lowers ocean freight costs per storage position and prevents internal container cargo shifting during transoceanic transit.
| Destination Market | Primary Discharge Ports | Indicative Sea Transit Time* | Recommended Surface Finish | Standard Shipping Terms |
|---|---|---|---|---|
| Vietnam | Haiphong / Cat Lai (Ho Chi Minh City) | 2 – 5 Days | Tropical Epoxy Powder Coat | FOB / CIF / CFR |
| Philippines | Manila South / North Harbor, Batangas | 3 – 5 Days | Reinforced Seismic Anchor + Epoxy | FOB / CIF / DDP |
| Thailand | Laem Chabang / Bangkok Modern Terminal | 5 – 7 Days | Epoxy Powder Coat / Galvanized | FOB / CIF |
| Singapore | Port of Singapore Authority (PSA) | 5 – 7 Days | Premium High-Gloss Epoxy Coat | FOB / CIF / DDU |
| Malaysia | Port Klang (North / West Port) / Penang | 6 – 8 Days | Tropical Epoxy Powder Coat | FOB / CIF / DDP |
| Indonesia | Tanjung Priok (Jakarta) / Tanjung Perak | 7 – 10 Days | Seismic Reinforced + Epoxy | FOB / CIF |
| Middle East & Europe | Jebel Ali, Rotterdam, Hamburg, Valencia | 18 – 30 Days | Heavy-Duty Industrial Powder Coat | FOB / CIF / CFR |
*Note: Indicative port-to-port maritime shipping durations from South China. Exact transit times depend on vessel liner schedules, seasonal monsoons, and local customs clearance speed.
Frequently Asked Questions on Sourcing Warehouse Roller Racks
Detailed technical, operational, and commercial answers prepared by HEDA senior project engineers to help procurement teams make informed, risk-free purchasing decisions.
The incline angle is governed by the weight of the load, the stiffness of the carton bottom or pallet base, the roller track wheel diameter, and the ambient temperature. For standard e-commerce carton flow picking (totes and rigid cartons weighing between 5 kg and 35 kg), we recommend an incline of 2.5° to 3.5° (approximately a 4.5% to 6% gradient). If corrugated cartons have softer bases that sag between wheels, the slope angle may be increased by 0.5°, or high-density full-width rollers can be used to prevent deflection.
For heavy pallet gravity flow (500 kg to 1,500 kg), the required slope is lower: between 1.5° and 2.5° (approximately 3% to 4.5%). To maintain safe speeds, centrifugal speed controller rollers are mounted at one-pallet intervals along the lane. HEDA Shelves conducts physical roll-testing with customer sample cartons in our Guangzhou engineering workshop before shipping to guarantee optimal roll velocity.
Aluminum fluent strips utilize high-strength extruded aluminum alloy framing paired with high-impact POM (polyoxymethylene) or ABS plastic skate wheels. They offer exceptional weight-to-strength ratios, resist corrosion in moist climates, and support loads of 50 kg to 120 kg per linear meter, making them ideal for light-to-medium carton flow, retail picking, and electronic parts storage.
Heavy-duty steel roller tracks utilize cold-rolled galvanized steel C-channels and zinc-plated cylindrical steel rollers with precision steel ball bearings. These systems can carry loads exceeding 500 kg to 2,000 kg per lane, making them suited for automotive sub-assemblies, heavy tooling, industrial casting storage, and multi-tier pallet flow racks.
Moisture and coastal salt air pose serious corrosion risks to warehouse steelwork. At HEDA Shelves, all steel components undergo a thorough 9-stage pre-treatment process: alkaline degreasing, twin water flushes, acid pickling to eliminate mill scale, neutralization, and an iron-zinc phosphate chemical conversion dip that creates an inorganic barrier against moisture.
Components are then coated with an automated electrostatic thermoset polyester-epoxy powder layer (thickness: 60 to 80 microns) and cured in a 200°C baking furnace. For humid, coastal, or sub-zero cold-chain installations, we offer hot-dip galvanized finishes complying with ISO 1461, ensuring over 20 years of rust-free service life under high relative humidity.
Yes. Our carton flow and sliding rolling racks are designed with pre-punched cable management raceways and dedicated mounting extrusions on the front beam profile to support major Pick-to-Light (PTL), Put-to-Light, and electronic shelf label (ESL) systems. We can also provide integrated carton-sensing micro-switches or photoelectric sensors at the pick face that trigger automated inventory decrement signals to your WMS whenever an operator removes a carton.
To generate an accurate AutoCAD layout, 3D rendering, and quotation, our structural engineering department requires: 1. Warehouse building architectural floor plans showing clear internal ceiling heights, column grids, fire exit routes, and sprinkler drop clearances. 2. Stored unit dimensions: length, width, height, and gross weight (minimum, average, and maximum per carton or pallet). 3. Packaging type: corrugated paper boxes, rigid plastic tote bins, wooden Euro/GMA pallets, or metal skids. 4. Daily throughput requirements: replenishment rates, pick frequencies, and SKU counts per bay. 5. Material handling equipment: forklift types, clear mast lift heights, and turning radii. Our team delivers a comprehensive layout proposal and load calculation analysis free of charge within 24 to 48 hours.
Every international export order from HEDA Shelves includes a comprehensive engineering handover package: high-resolution 3D assembly exploded diagrams, numbered component identification tags corresponding to shipping packing lists, and step-by-step video installation walk-throughs. Upright frames are typically shipped pre-bolted to accelerate field assembly.
For large-scale distribution centers and multi-tier mezzanine roller projects, HEDA can dispatch certified bilingual installation engineers to your job site to oversee contractor teams, verify anchor torque tightness, calibrate roller track pitch angles, and conduct final dynamic commissioning tests before official facility handover.
Ready to Maximize Your Warehouse Floor Space & Picking Velocity?
Consult directly with HEDA Shelves project engineers. Submit your warehouse floor plan dimensions and SKU specifications today to receive a custom CAD layout, 3D simulation rendering, and competitive factory-direct quote within 24 to 48 hours.