Industrial High Bay Racking Systems & Space Optimization
Precision roll-formed cold steel profiles compliant with ISO 9001:2015, CE EN 15512, and RMI (Rack Manufacturers Institute) standards. Designed for high clearance logistics warehouses reaching up to 30 meters.
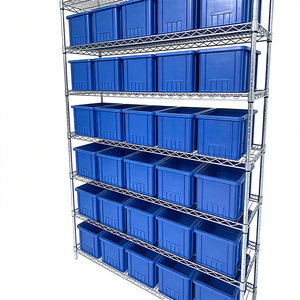
High Quality 7 Layers 250kgs Heavy Duty Factory Warehouse Metal Storage Rack Shelving
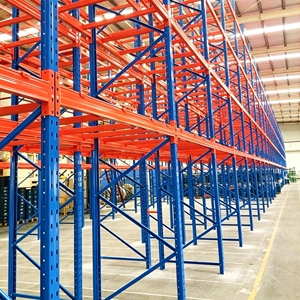
Hot Selling Adjustable Heavy Duty Steel Industrial Racks 6 8 10 Layer High Bay Pallet Racking
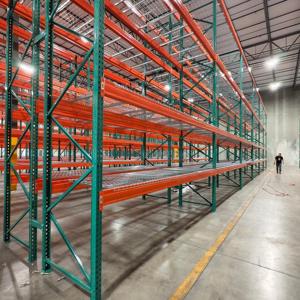
Jracking US Inventory Warehouse Stacking Shelves Heavy Duty Teardrop Pallet Racking System
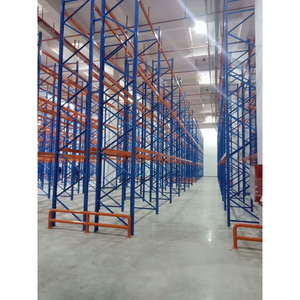
Blue-Orange High Bay Heavy Duty Racking Adjustable Easy Assemble Storage Solution
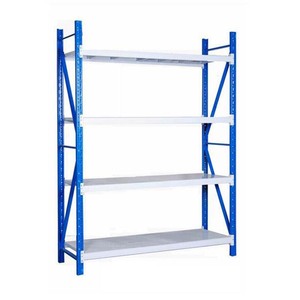
Longspan Shelving Rack High Bay Industrial Shelves Narrow Aisle Heavy Duty Pallet Racking
Metal Warehouse Building High Bay Facility Pallet Rack Logistics Optimization System
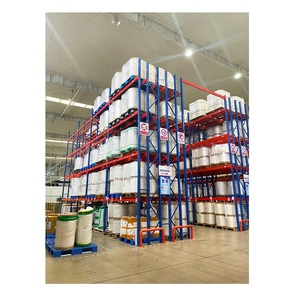
Pallet Racking System Industrial High Bay Double Deep Heavy Duty Selective Storage Rack
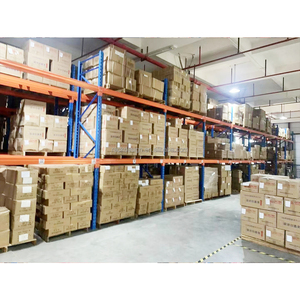
Warehouse Disassembled Industrial Rack High Bay Selective Heavy Duty Pallet Rack Systems
Structural Integrity & Material Benchmarks for High Bay Logistics
Evaluating structural load-bearing parameters, finite element analysis (FEA), and Chinese steel metallurgic standards for multi-tier vertical storage infrastructure.
| Engineering Parameter | HEDA High Bay Standard | Generic Market Spec | Strategic Impact on Logistics Operations |
|---|---|---|---|
| Primary Steel Grade | Q235B / Q355B (Cold Rolled) | Recycled Low-Carbon Scrap / Q195 | High tensile yield strength (up to 355 MPa) eliminates progressive collapse risks in bays exceeding 12m height. |
| Column Upright Section | 90mm–140mm omega profiles (11–13 fold) | Standard 70–80mm roll profiles (5–7 fold) | Advanced multi-faceted roll profiling maximizes structural moment of inertia and resistance to lateral torsional buckling. |
| Deflection Limit Standard | 1/200th of clear span beam (FEM 10.2.02) | 1/150th or unrated | Eliminates automated shuttle and reach-truck mast binding when lifting pallets at elevations above 10,000mm. |
| Surface Pre-Treatment | 9-stage pickling, phosphating & passivation | Simple degrease wash & air dry | ASTM B117 salt spray test rating > 500 hours; 100% rust prevention in high-humidity tropical or coastal climates. |
| Powder Coating Chemistry | Electrostatic thermoset polyester (70–90µm) | Mixed epoxy-hybrid (40–50µm) | Exceptional resistance to chipping from high-frequency forklift fork impacts; meets RoHS and environmental non-toxicity. |
| Seismic Damping Compliance | Tailored bracing per UBC / IBC Zone 4 | Non-seismic static rating only | Includes baseplate floor anchoring with heavy sleeve chemical anchors engineered for earthquake-prone geographies. |
FEA Load Distribution Verification
All custom upright frames and box step beams undergo computerized finite element analysis (FEA). This simulates full load stresses, pallet impact shocks, and cyclic fatigue, guaranteeing zero catastrophic joint failure under rated loads.
Dynamic Deflection Tolerance
High bay racking systems require rigorous horizontal drift limits. Our structures adhere to European FEM 10.2.02 and American RMI specifications, keeping total lateral deflection under 1.5% under dynamic automated crane operations.
Integrated Safety Accessories
Every high-bay solution integrates impact column guards, guide rail networks for VNA wire or optical guidance, heavy-duty backstop beams, and anti-collapse wire mesh containment screens to safeguard floor personnel.
Guangzhou HEDA Shelves: Advanced Manufacturing Powerhouse
Established in 2001, Guangzhou Heda Shelves Co., Ltd. operates state-of-the-art intelligent manufacturing facilities delivering CE (No. 2435-CPR-8605159) and ISO 9001:2015 certified heavy-duty storage infrastructure globally.
10-Stage In-House Quality Controlled Manufacturing Sequence
Unlike assemblers who outsource critical components, HEDA controls 100% of the manufacturing value chain under one roof, guaranteeing structural integrity from coil slit to final packing.
Certified Coils
Premium Q235B/Q355B prime hot-dip & cold-rolled carbon steel coils.
Laser Slitting
High-speed laser cutting & CNC multi-axis automatic slit shearing.
Automated Punch
Continuous CNC stamping for 50mm/75mm/teardrop pitches (±0.1mm tolerance).
Cold Bending
Progressive multi-roll forming stations creating stable omega profile ribs.
Profile Forming
Precision roll-forming of interlocking box step beams and upright braces.
Robotic Welding
Multi-axis automated gas-shielded welding of beam connectors and footplates.
Shot Blasting
Mechanical surface descaling to reach SA 2.5 standard for optimal adhesion.
Phosphating
Full-immersion chemical cleaning, acid pickling, rust removal, and sealing.
Powder Coating
Automated Swiss Gema electrostatic powder coat lines cured at 200°C.
QC & Bundling
Dimensional laser scan, load verification, palletized export container packaging.
Future Procurement Trends in High Bay Warehouse Systems
How industrial developers, third-party logistics (3PL) giants, and manufacturing plants are adapting their global procurement blueprints for the 2026–2030 cycle.
1. Convergence of Very Narrow Aisle (VNA) and Automated Radio Shuttles
Skyrocketing industrial land lease rates across Southeast Asia, North America, and Europe have rendered traditional 3.5-meter wide forklift aisles uneconomical. Procurement directors are systematically shifting budgets toward Very Narrow Aisle (VNA) systems requiring only 1.6m–1.8m aisles, combined with high-speed automated four-way radio shuttles.
Procurement teams are demanding that racking uprights be pre-engineered with precision running tracks, proximity sensor mounts, and high-tolerance floor anchoring channels to enable seamless retrofitting from manual VNA trucks to autonomous guided vehicles (AGVs).
- Up to 85% Volumetric Space Utilization: Compressing aisle real estate directly cuts warehouse overhead per pallet footprint.
- Total Cost of Ownership (TCO) Prioritization: Buyers look beyond initial steel tonnage price, factoring lifecycle durability and field maintenance costs.
Procurement Metric: Steel Weight vs. Structural Rigidity
Modern engineering replaces brute steel thickness with intelligent geometry. High-tensile Q355B cold-rolled profiles with multi-point omega bending deliver equal or superior moment of inertia with up to 14% less raw steel deadweight, slashing international sea freight costs.
2. Cold Chain Resilience & Microclimate Racking Coatings
With the rapid expansion of global pharmaceutical logistics and frozen perishable food distribution, high bay storage inside sub-zero environments (-25°C to -30°C) is booming. Sub-zero thermal contraction causes conventional paint finishes to micro-crack, introducing moisture condensation and rapid subsurface steel oxidation.
Procurement trends demonstrate a dramatic surge in demand for specialized hot-dip galvanized (HDG) beam components and elastic epoxy-polyester coatings enriched with anti-microbial additives. Chinese factories capable of offering verified cyclic humidity testing are taking the lead in worldwide cold storage tenders.
- Zero Delamination Formulations: Elasticized powder resins withstand sudden thermal shocks during defrost cycles.
- Perforated Airflow Decking: Facilitates even temperature distribution across dense frozen inventory blocks.
Direct Container Loading Optimization
High bay upright frames exceed standard 40HQ container interior lengths (11.8m). Advanced Chinese manufacturers solve this bottleneck using structural splice joints designed to maintain 100% moment transfer while fitting standard maritime container cubes, saving up to 40% in international breakbulk shipping costs.
Technological Breakthroughs Transforming High Bay Racking
From structural health IoT monitoring to digital twin integration, discover how China’s top racking factories are elevating static steel structures into intelligent logistics assets.
Digital Twin & BIM Structural Modeling
Modern high-bay projects are engineered using complete Building Information Modeling (BIM) workflows. Engineers export LOD-400 structural models directly into warehouse management software (WMS), allowing project managers to detect physical building clashes, sprinkler pipe clearances, and lighting intrusions prior to on-site installation.
Embedded Strain Gauge & Overload Sensors
Smart high bay racking frames are increasingly equipped with embedded piezoelectric strain sensors along critical lower upright columns. These IoT devices communicate wirelessly with the plant's maintenance portal, issuing real-time alerts if a forklift collision compromises column geometry or if weight exceeds permissible design thresholds.
Seismic Dissipation & Base Isolation Damping
In seismically active zones such as Japan, the Philippines, Indonesia, and the US West Coast, high bay racks act as tall cantilevered masses. Cutting-edge factories now incorporate high-ductility elastomeric base isolators that absorb ground shear waves, preventing upright buckling and shelf load ejection during seismic tremors.
Frequently Asked Questions by Industrial Sourcing Directors
Clear, verifiable answers regarding manufacturing standards, international logistics, installation tolerances, and custom engineering.
What floor slab tolerances are mandatory before erecting high bay racks?
High bay racking systems exceeding 10 meters require strict concrete floor slab superflatness complying with DIN 18202 Table 3 (Group 4) or ACI F-min 75 to 100 specifications. Slab deflection must not exceed 1/500th of column spacing under maximum dual-sided pallet loads to avoid dynamic reach truck mast binding.
How do you guarantee quality consistency across large orders (e.g., 50+ containers)?
HEDA enforces strict ISO 9001:2015 quality control checklists at every production checkpoint. Raw steel coils are tested for chemical composition (Carbon, Manganese, Silicon) and yield strength before slitting. Roll-formed sections undergo laser profile scanning every 500 meters to ensure dimensional variances remain within ±0.3mm.
Can your racking systems integrate with third-party automated crane (ASRS) vendors?
Yes. Our high bay uprights and support beams are engineered to integrate with European, American, and Asian crane vendors (such as Dematic, Swisslog, Daifuku, and Honeywell). We provide precision-machined top guide rail assemblies, optical reflector mounts, and specialized rail anchoring systems engineered to tight millimeter clearances.
What engineering data is required to provide a formal CAD layout and quotation?
To receive a verified structural proposal, provide: warehouse architectural drawings (DWG/PDF) highlighting clear ceiling heights and column grids; pallet dimensions (W × D × H including overhang); maximum gross weight per pallet; forklift model and maximum lift height; and any local seismic acceleration coefficients (Ss, S1).
How does the factory prevent corrosion during ocean shipping across tropical zones?
In addition to 9-stage chemical phosphating and high-density polyester powder coating, export shipments feature heavy vapor corrosion inhibitor (VCI) shrink wrap, desiccants inside every bundled bundle, and specialized wooden base runners that prevent steel-on-steel friction and maritime saltwater aerosol infiltration inside shipping containers.
What is the typical production and delivery lead time for high bay systems?
Standard production for customized 5 to 20-container high-bay facilities takes approximately 20 to 30 working days from drawing sign-off. Direct shipping from Guangzhou or Nansha port offers fast sea transit times: 2–5 days to Vietnam, 5–7 days to Singapore/Thailand, 14–18 days to the Middle East, 18–25 days to Europe, and 20–28 days to the US West Coast.
How are structural upright frames over 11.8m shipped inside standard ocean containers?
For high bay warehouses from 12m to 30m, HEDA engineers high-strength bolted splice joints. The internal splice sleeves are laser-cut from high-yield Q355B structural steel and fixed with Grade 8.8 structural bolts. This design preserves complete structural moment capacity while allowing components to ship securely inside standard 40-foot high-cube containers.
Do you offer on-site installation guidance and overseas engineering support?
Every project includes 3D isometric assembly blueprints, numbered component manifests, and high-definition installation video tutorials. For major industrial installations, HEDA can deploy certified bilingual installation supervisors and commissioning engineers to manage local contractor teams on-site until final project handover.
Ready to Maximize Your High Bay Warehouse Footprint?
Connect directly with Guangzhou HEDA’s senior structural design team. Receive a complimentary 2D CAD spatial layout, 3D visualization render, and detailed structural bill of materials (BOM) within 24 hours.