Featured Industrial Warehouse & Pallet Flow Racking Systems
High-performance material handling systems manufactured to tight structural tolerances, optimized for high-density FIFO stock turnover, heavy industrial loads, and fast order fulfillment.
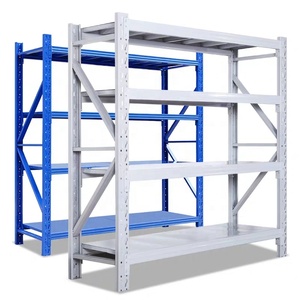
Mracking Adjustable Boltless Racks Industrial Light Duty Shelf Pallet Shelving
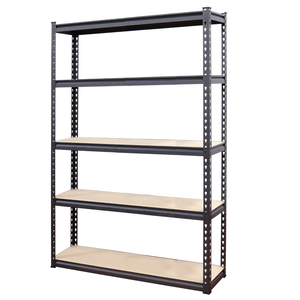
5 Tier Storage Shelving 1.5mm Boltless Carbon Steel Frame 12mm MDF Shelf Board
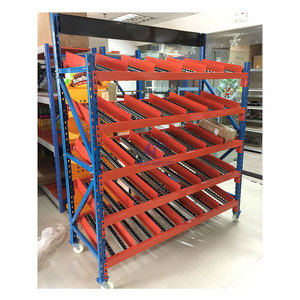
Customized Warehouse Storage Rack Pallet Flow Rack Lineside Gravity Flow Racking
Long-term Reserve Special Stable Metal 5-Layer Heavy Duty Storage Rack
Factory Direct Supply Durable Heavy Duty Industrial Steel Plate Storage System
Heavy Duty Double Deep Steel Pallet Racking System Adjustable Beam Storage
Custom Heavy Duty Industrial Steel 5 Multi-Level Carpet Roll Storage Racks
Narrow Aisle Racks Factory Price Heavy Duty VNA High Density Storage Rack
The Engineering Mechanics of Gravity Pallet Flow Racks
Gravity flow racking represents the pinnacle of passive dynamic automation. Operating purely on controlled gravitational forces, an engineered gravity flow system transforms deep storage cubic volume into a dynamic FIFO conveying circuit.
Slope Gradient Calibration (3.5%–4%)
The kinetic baseline of gravity flow relies on a mathematically defined pitch angle—typically between 3.5% and 4% (approximately 1.5 to 2.3 degrees). If the angle is below 3%, pallet friction creates static hang-ups; if exceeding 4.5%, momentum causes severe terminal impact risks.
Kinetic Gradient: ~3.5% PitchCentrifugal Speed Controller Rollers
Without mechanical deceleration, a 1,200 kg pallet traveling down a 30-meter deep lane would reach catastrophic speeds. Integrated centrifugal magnetic or gear-governed brake rollers automatically engage as velocity rises, restricting pallet progression to a safe 0.15 to 0.3 m/s.
Speed Limit: <0.3 m/s ConstantLine-Pressure Pallet Separators
In deep-lane configurations (up to 20 pallets deep), cumulative hydraulic back-pressure makes forklift removal unsafe. Patented mechanical separation stops isolate the lead pallet from upstream queuing force, only cycling release mechanics after the retrieved pallet leaves the front discharge face.
Safety: Zero Back-Pressure ExtractionTop 10 Gravity Flow Racking System Factories & Suppliers
To aid global supply chain executives, industrial architects, and procurement leads, our engineering research group has evaluated the world's leading gravity flow racking manufacturers based on metallurgical integrity, test track accuracy, lead-time control, and direct factory pricing.
| Rank / Supplier | Headquarters | Manufacturing Scale | Key Strengths & Roller Systems | Primary Certifications | ASEAN / Global Delivery |
|---|---|---|---|---|---|
|
1
Guangzhou HEDA Shelves Co., Ltd.
|
Guangzhou, China | 30,000 m² | 30,000 t/mo | Direct factory pricing, custom brake roller tracks, anti-corrosive powder finish | CE, ISO 9001:2015, RoHS | 2–10 Days Sea Transit (ASEAN Hubs) |
|
2
Interroll Group
|
Sant'Antonino, Switzerland | Global Tier 1 (15+ Plants) | Pioneering roller tracks, Magnetic Speed Controllers (MSC 50), high modularity | ISO 9001, CE, TÜV | Global Distribution Network |
|
3
Mecalux, S.A.
|
Barcelona, Spain | 11 Production Centers | High-rise automated integration, heavy-duty gravity flow lines, software syncing | ISO 9001, EN 15512 | Europe & Pan-American Focus |
|
4
SSI SCHAEFER
|
Neunkirchen, Germany | Global Megafactories | Carton flow & pallet flow modules, turnkey intralogistics ecosystems | ISO 9001, ISO 14001, CE | Worldwide Direct Representation |
|
5
BITO-Lagertechnik Bittmann
|
Meisenheim, Germany | Specialist European Plant | Robust roller tracks, precision pick-face carton flow, cold-room expertise | RAL-RG 614, CE | European & Selected Asian Hubs |
|
6
Dematic (KION Group)
|
Atlanta, GA, USA | Global Production Footprint | Heavy automation integration, dynamic lineside gravity feeds for AGVs | ISO 9001, ANSI/RMI | Global Automation Projects |
|
7
Stow Group
|
Dottignies, Belgium | 9 European Facilities | Stow Atlas racking compatibility, deep-lane gravity pallet flow channels | EN 15512, ISO 9001 | EMEA & Emerging Americas |
|
8
Nedcon B.V.
|
Doetinchem, Netherlands | Specialized European Mill | Complex high-bay structural flow engineering, tight seismic load tolerance | ISO 9001, EN 1090 | Europe & International Projects |
|
9
Steel King Industries
|
Stevens Point, WI, USA | 4 Manufacturing Plants | Heavy tubular welded uprights, severe forklift impact resistant flow frames | RMI Certified, ANSI MH16.1 | North America Centric |
|
10
Advance Storage Products
|
Huntington Beach, CA, USA | 2 US Facilities | Specialized deep-lane flow, "Lo-Pro" push-back and pallet flow engineering | RMI Certified, ISO | North America & Export Ports |
1. Guangzhou HEDA Shelves Co., Ltd.
Guangzhou, ChinaFounded in 2001, HEDA Shelves has emerged as an authoritative global leader in custom-engineered warehouse racking, boasting a 30,000 m² state-of-the-art manufacturing plant in Guangzhou with a 30,000-ton monthly capacity. Uniquely combining mill-direct pricing with rigorous structural engineering, HEDA provides complete OEM/ODM gravity flow systems featuring custom roller beds, speed retarders, and anti-corrosive multi-stage pre-treatments (pickling and phosphating) ideal for tropical and cold-chain environments.
2. Interroll Group
SwitzerlandInterroll is globally recognized as the benchmark manufacturer for dynamic conveying components. Their pallet flow division provides precision roller tracks, universal magnetic speed controllers, and time-tested mechanical separation systems. While predominantly supplying system integrators rather than direct rack upright fabrication, their roller modules are considered the gold standard for high-throughput, mission-critical distribution centers.
3. Mecalux, S.A.
SpainOperating 11 manufacturing plants across Europe and the Americas, Mecalux is a storage titan recognized for turnkey dynamic racking systems. Their gravity flow solutions excel in live storage configurations requiring integration with complex Warehouse Management Systems (Easy WMS). Their systems feature robust structural steel profiles and split-roller designs to handle uneven wooden pallets.
4. SSI SCHAEFER
GermanyA premier German intralogistics conglomerate, SSI Schaefer engineers both carton flow and heavy pallet live storage systems. Known for extreme dimensional precision, their live storage beds seamlessly connect with picking mezzanines and automatic guided vehicles (AGVs). Their offerings carry a premium price tag, tailored for Fortune 500 distribution operations.
5. BITO-Lagertechnik Bittmann GmbH
GermanyBITO specializes in live storage engineering with a strong focus on order picking efficiency. Their carton flow systems feature multi-ribbed plastic and steel rollers with ergonomic drop-in pick trays, while their heavy pallet live storage utilizes heavy-gauge channel frames with integrated entry guides to prevent forklift misalignment in high-pace FMCG depots.
6. Dematic (KION Group)
USA / GermanyAs an automation powerhouse under the KION umbrella, Dematic utilizes gravity flow racking primarily as high-velocity buffer lines between manufacturing assembly and outbound shipping docks. Dematic's dynamic gravity lanes are equipped with extensive sensor tracking, telemetric speed governing, and automated pallet-release triggers.
7. Stow Group
BelgiumStow is one of Europe's largest racking producers, renowned for cold-formed steel manufacturing. Their dynamic pallet live storage systems feature standardized clip-on roller track assemblies that integrate directly into their standard Stow uprights and beam profiles, providing exceptional modular flexibility and rapid field installation.
8. Nedcon B.V.
NetherlandsNedcon is celebrated in the structural logistics domain for engineering highly customized, seismically validated pallet flow systems. Operating with high-tensile European steel alloys, Nedcon calculates exact deflection ratios for multi-tier flow rack configurations where high-density gravity channels are mounted directly onto complex picking mezzanines.
9. Steel King Industries
USAA leader in North American structural storage, Steel King is famed for its rugged structural tubular steel uprights. In gravity flow installations, their tubular column construction resists severe lift-truck impacts at loading and unloading faces, making them a preferred choice for heavy manufacturing plants and grocery distribution hubs.
10. Advance Storage Products
USAAdvance Storage Products specializes heavily in high-density dynamic systems, including their patented deep-lane pallet flow lines. Their systems utilize continuous structural channel frames, reinforced entry guides, and multi-track roller arrangements engineered specifically to accommodate variable quality GMA wood pallets.
Guangzhou HEDA Shelves: Engineered Racking Manufacturing Since 2001
For procurement directors, distributors, and logistics engineers seeking the optimal balance between high-grade metallurgical engineering and factory-direct cost containment, Guangzhou HEDA Shelves Co., Ltd. stands out as the premier direct Chinese manufacturing partner.
Complete in-house manufacturing: precision steel slitting, automated CNC column punching, roll forming, robotic welding, and high-efficiency powder coating lines.
Every beam and upright undergoes automated industrial pickling and phosphating pre-treatment before electrostatic powder deposition, ensuring 80%+ humidity resilience.
In-house structural engineers calculate seismic resistance, clear height tolerances, and forklift turning radiuses, delivering verified drawings free of charge.
Strategic Guangzhou port location ensures direct sea transit of 2–5 days to Vietnam, 3–5 days to Manila, 5–7 days to Singapore/Laem Chabang, and 6–8 days to Port Klang.
Global tenders and multinational procurement standards require incontrovertible quality credentials. HEDA Shelves components are manufactured strictly in accordance with European standard EN 15512 and ISO protocols, rigorously load-tested under third-party supervision.
Future Procurement & Technological Trends (2026–2030)
The gravity flow racking landscape is transforming rapidly under the pressures of e-commerce SKU proliferation, rising warehouse real estate costs, and zero-carbon sustainability mandates.
Bypassing Intermediaries for Direct Factory OEM
Supply chain leaders increasingly disintermediate local distributors, partnering directly with large-scale factories capable of custom roll-forming. This eliminates 20–35% markups and enables direct engineering modifications for non-standard pallets.
Lifecycle Costing vs. Initial Capital Expense
Procurement teams are prioritizing roller bearing longevity, galvanized durability, and modular replacement over cheap upfront bids. Unplanned downtime caused by seized brake rollers in high-bay live lanes costs far more than premium roller assemblies.
Seismic and Microclimate Specific Procurement
Warehouse planners in tectonic zones (the Philippines, Indonesia, western Americas) mandate location-specific structural FEA calculations, specifying enlarged baseplates, heavy floor anchoring, and dynamic slope retention locks.
Self-Powered Smart Sensor Rollers & IoT Telemetry
Next-generation dynamic beds integrate micro-dynamo rollers that generate telemetry data from pallet movement, tracking inventory fill rates, deceleration consistency, and roller bearing wear directly into warehouse management software.
Hybrid AMR / AGV Lineside Gravity Interfaces
Gravity flow is transitioning from traditional forklift access to automated interfaces. Low-angle lineside carton and pallet flow racks are now designed with cantilevered discharge trays accessible by autonomous mobile robots (AMRs).
Zero-Energy Passive Cold-Chain Logistics
With refrigerated warehouse electricity costs spiking globally, live gravity flow is rapidly replacing powered automated storage and retrieval systems (ASRS) in sub-zero freezers, utilizing zero power while eliminating forklift cold-room dwell time.
Gravity Flow Racking Procurement & Engineering FAQ
Detailed engineering answers to critical architectural and procurement inquiries commonly encountered during facility design.
Q: What is the critical difference between full-width rollers and twin-track skate wheel flow beds?
Full-width cylindrical steel rollers support bottom-board configurations across the entire pallet span, making them mandatory for variable quality wood pallets, heavy loads (>800 kg), and uneven runners. Twin-track or multi-track skate wheels work well only for uniform plastic pallets or standardized GMA/Euro pallets with clean, rigid bottom boards. For heavy industrial use, full-width rollers minimize point-load deformation.
Q: How do you prevent catastrophic "runaway pallet" acceleration in deep lanes?
Acceleration control is achieved through engineered placement of centrifugal brake rollers. Typically, one brake roller is installed per pallet position along the flow channel. When a pallet rolls over the retarder, an internal planetary gear or magnetic mechanism engages, absorbing excess kinetic energy and keeping descent velocity at a controlled, safe 0.2 to 0.3 m/s.
Q: Can gravity flow racking operate safely in sub-zero cold storage (-25°C to -30°C)?
Yes, but it requires cold-rated engineering specifications. Roller bearings must use synthetic low-temperature lubricants that do not solidify. Steel components should undergo hot-dip galvanization or zinc-rich coatings to resist condensation corrosion, and brake retarders must feature sealed fluidless magnetic mechanisms to prevent internal freezing.
Q: What parameters are needed by the factory to calculate the exact lane gradient?
The factory engineering team requires: (1) Minimum and maximum gross weight per pallet; (2) Pallet dimensions and bottom deckboard orientation (crosswise vs lengthwise to flow); (3) Pallet material and construction quality; (4) Total storage depth (number of pallets per lane); and (5) Operating ambient temperature. Test-rolling samples on an adjustable factory rig is standard protocol for mission-critical orders.
Q: How does line pressure separation protect forklift operators during unloading?
In a 10-pallet deep lane with 1,000 kg pallets, the static pressure on the front discharge pallet reaches several tons. Without separation, the front pallet is jammed hard against the end-stop, risking load collapse and making fork entry hazardous. An automatic mechanical pallet separator holds back the 2nd through 10th pallets until the lead pallet is lifted clear, eliminating all back-pressure.
Q: What documentation and certifications should be mandated in international tenders?
International tenders should require CE certification (EN 15512 compliance for structural racking), ISO 9001:2015 for quality control, mill certificates confirming Q235B or Q355B structural steel grade, third-party structural load calculation reports, and salt spray test reports (ASTM B117) verifying minimum 500-hour corrosion resistance for powder-coated finishes.
Transform Your Warehouse Density with Precision Gravity Flow Engineering
Consult directly with HEDA Shelves' senior logistics engineers. Share your building layout, pallet dimensions, and SKU throughput for a complimentary CAD optimization plan, 3D render, and direct factory quote.