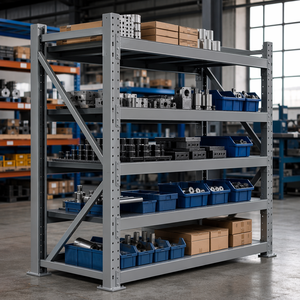
 Heavy-Duty Frame
Custom OEM Storage Rack Frame | Heavy Duty Steel Welded Fabrication for Warehouse Pallet Racking
Q235B / Q355B Steel
Custom Upright Pitch
Engineered for intense load distribution, high turnover ratios, and heavy-duty seismic resistance. Explore standard and customizable modules ready for factory-direct dispatch.
Heavy-Duty Frame
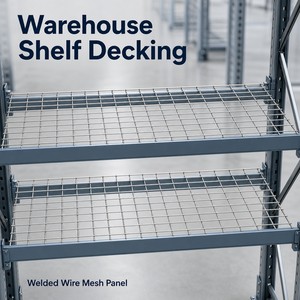 Safety Decking
 Facility Infrastructure
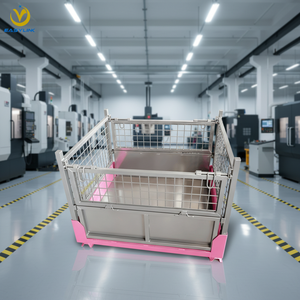 Material Handling
 Dynamic Gravity Flow
 2000kg Capacity
 Space Expansion
 Modular Stacking
Gravity feed pallet racking, universally designated in industrial intralogistics as Pallet Flow Racking or Dynamic Live Storage, operates on an unpowered, sloped roller track mechanism that harnesses earth's natural gravitational vector. Unlike static selective pallet systems requiring continuous forklift aisle navigation, gravity systems segregate loading and unloading operations into two dedicated, opposed aisles. Pallets are inducted at the elevated charging face (incline pitch ranging from 2.5% to 4%, typically 1.5° to 2.3°), navigate an engineered roller track bed under controlled acceleration, and arrive seamlessly at the discharge face for high-speed retrieval.
This strict physical segregation ensures uncompromising First-In, First-Out (FIFO) stock rotation, making it the premier architectural standard for temperature-controlled cold chains, high-velocity pharmaceutical fulfillment centers, fast-moving consumer goods (FMCG) distribution buffers, and food processing plants facing strict batch integrity and expiry control mandates.
To eliminate pallet runaway catastrophic structural failure, high-precision engineering must balance kinetic energy dissipation across extended lane depths (often spanning 2 to 25 pallets deep). Industrial gravity flow racks depend on three mission-critical mechanical subsystems:
Integrated directly within the roller track bed at calculated intervals (typically every 1 pallet position), internal planetary gearboxes utilize centrifugal friction clutches. When a traversing pallet accelerates beyond safe velocity (exceeding 0.25 to 0.3 m/s), internal flyweights expand against brake drums, maintaining a constant, safe coasting velocity regardless of total pallet payload weight (from 300 kg up to 1,500 kg).
In deep-lane configurations, dynamic hydrostatic pressure accumulates at the discharge face. An engineered floor-level mechanical pallet separator isolates the front extraction pallet from the rear queued line by a physical 150-200mm gap. This completely relieves backpressure, allowing forklift operators to extract the pick pallet effortlessly without friction jamming or vehicle hydraulic damage.
Constructed from reinforced structural steel angle profiles equipped with high-durometer polyurethane elastomer bumpers, end stops absorb the terminal docking kinetic shock of fully loaded pallets. Heavy-gauge anchor base plates distribute shear loads directly into the concrete floor slab, preserving upright column structural integrity against cumulative fatigue wear.
A comparative architectural evaluation of global tier-1 racking manufacturers versus direct-from-source engineering fabrication powerhouses based on engineering depth, structural steel compliance, and cost-to-performance ratio.
Selecting an industrial gravity flow racking partner requires rigorous technical evaluation. While European and American integrators provide brand prestige, Asian direct-manufacturing tier-1 giants like Guangzhou HEDA Shelves Co., Ltd. have re-engineered the global supply chain by coupling precision OEM roll-forming and welding fabrication with rapid lead times and direct-from-mill pricing.
| Manufacturer / Supplier | Primary Manufacturing Hub | Core Flow Racking Strengths | Certification & Compliance | Sourcing Advantage |
|---|---|---|---|---|
| HEDA Shelves (Guangzhou HEDA Shelves Co., Ltd.) | Guangzhou, China (30,000 m² Plant) | Custom heavy-duty roller tracks, deep lane flow systems, integrated mezzanine & push-back racking | CE, ISO 9001:2015, RoHS | Direct factory pricing, custom OEM/ODM, 2-10 days sea transit to ASEAN, free 3D/CAD structural design |
| SSI Schaefer | Neunkirchen, Germany / Global | Fully integrated high-throughput automated logistics, live storage pick tunnels | EN 15512, ISO 9001, FEM 10.2.02 | Turnkey global systems integration for ultra-large automated logistics parks |
| Bito-Lagertechnik Bittmann GmbH | Meisenheim, Germany | Precision carton and pallet flow tracks, proprietary twin-roller assemblies | RAL-RG 614, ISO 9001, CE | High mechanical refinement in pharmaceutical cleanroom and cold-chain sectors |
| Interroll Group | Sant'Antonino, Switzerland | Proprietary magnetic speed controllers, modular dynamic roller beds | CE, ISO 9001, UL Listed | Industry-leading roller and drive component sub-assembly supplier to worldwide OEMs |
| Mecalux, S.A. | Barcelona, Spain / USA / Poland | Extensive pallet flow and automated AS/RS warehousing integration | ISO 9001, ISO 14001, RMI Certified | Robust European and American warehouse distribution logistics footprint |
| Stow Group (Averys) | Spiere-Helkijn, Belgium | Standardized structural rack frames, high-bay dynamic live storage | EN 15512, ISO 9001 | High structural strength profiles suited for extreme pallet weights |
| Jungheinrich AG | Hamburg, Germany | Integrated warehouse equipment, forklift-to-rack ergonomic flow interfaces | ISO 9001, FEM Compliant | Holistic ecosystem pairing MHE vehicles with storage racking infrastructure |
| Dexion (Gonvarri Material Handling) | Laubach, Germany / Romania | Custom pallet flow systems with advanced brake roller intervals | EN 15512, ISO 9001, ISO 14001 | Proven structural performance in challenging climate and distribution nodes |
| Frazier Industrial Company | Long Valley, NJ, USA | Structural steel channel racking, high impact resistance flow lanes | RMI Certified, AISC | Exceptional durability in rugged heavy industrial forklift environments |
| Nedcon (voestalpine Group) | Doetinchem, Netherlands | Engineered micro-tolerance modular live storage for system integrators | EN 15512, ISO 9001, CE | Specialized high-density dynamic storage for complex intralogistics systems |
Over 25 years of specialized structural fabrication, world-class steel processing, and verifiable certifications deliver heavy-duty performance at direct factory pricing.
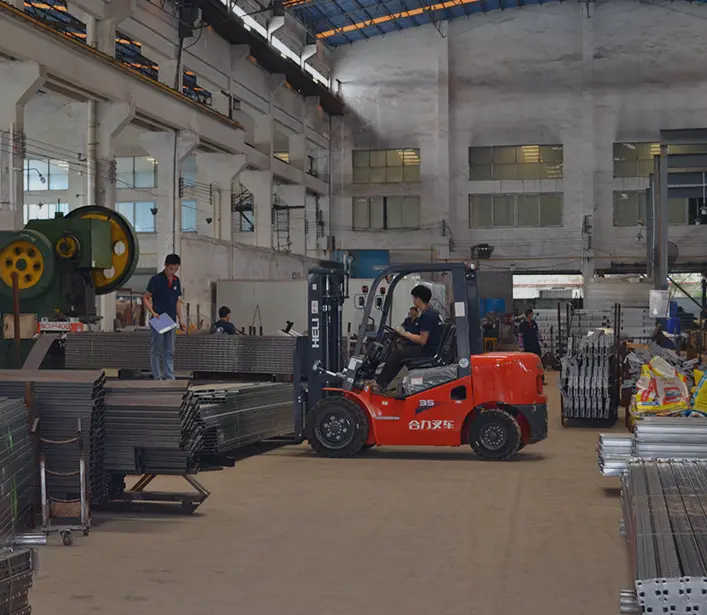
Founded in 2001, Guangzhou HEDA Shelves Co., Ltd. has grown into an international engineering powerhouse with over 300 experienced technical craftsmen, structural design engineers, and automated manufacturing specialists. Sourcing directly from HEDA provides unmatched advantages over standard trading companies and high-overhead global integrators:
Every upright, diagonal brace, and load beam is rolled from certified Q235B or high-tensile Q355B cold-rolled carbon steel coils, guaranteeing load deflection ratings well within standard L/200 thresholds.
To resist 85%+ relative humidity and harsh coastal climates in Southeast Asia, Latin America, and the Middle East, our 10-step finishing line applies an automatic pickling and phosphating pre-treatment followed by thermoset epoxy-polyester powder coating (60-90 μm thickness) or hot-dip galvanizing for cold storage longevity.
Tender with total confidence. HEDA Shelves holds official CE Certification (Certificate No. 2435-CPR-8605159) and ISO 9001:2015 Quality Management Accreditation (No. 18624Q00169R0M), ensuring full compliance with international safety and seismic codes.
Prior to production, our in-house engineering team calculates dead, live, wind, and seismic loadings to deliver comprehensive AutoCAD architectural layouts and 3D stress-analysis models at zero upfront charge.
Where intralogistics architecture meets material science. The five pivotal technological shifts dictating next-generation gravity feed pallet storage investments.
The physical boundary between gravity live storage and semi-automated radio shuttle carts is blurring. Future high-density facilities increasingly employ gravity flow lanes for automated buffering right behind Autonomous Mobile Robots (AMRs) or Automated Guided Forklifts (AGFs). This eliminates continuous electrical track powering while providing instantaneous, zero-latency pallet staging.
Traditional mechanical centrifugal brake rollers experience continuous internal pad wear and require maintenance cycles in abrasive cold or chemical environments. Next-generation gravity flow lanes are shifting toward sealed, permanent neodymium magnetic eddy-current controllers. These deliver completely contactless, non-wearing, maintenance-free deceleration unaffected by freezing frost, moisture, or chemical vapors.
With global supply chains transitioning from standard wooden Euro (1200x800) and GMA (48x40") pallets to plastic composite, steel skids, and slip-sheets with irregular underside runners, roller bed designs now incorporate triple-track staggered polyurethane wheel beds and universal continuous steel roller beds capable of moving defective or flexible pallet bottoms without snagging.
Modern mega-distribution hubs now demand predictive health sensing. Wireless vibration, bearing temperature, and cycle-count sensors embedded within end-stop buffers and critical brake rollers transmit telemetry directly to Cloud Warehouse Management Systems (WMS), alerting facilities to roller bearing fatigue before a lane blockage disrupts shipping schedules.
Green building mandates (LEED Gold, BREEAM) are imposing carbon tracking on warehouse hardware. Enterprise buyers prioritize mills utilizing electric arc furnace (EAF) low-carbon steel coils coupled with heavy-metal-free, zero-VOC powder coatings that deliver extreme salt-spray resistance (exceeding 500 hours under ASTM B117) with minimal environmental footprints.
In-depth technical answers addressing pallet tolerances, slope angles, cold store performance, seismic resistance, and international shipping.
Eliminate wasted forklift travel lanes, achieve strict FIFO inventory compliance, and boost cubic storage capacity by up to 60%. Connect directly with our senior intralogistics structural engineers for a complimentary CAD floor plan, dynamic 3D rendering, and factory-direct price quotation.