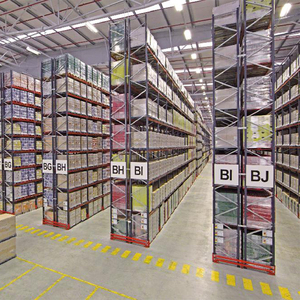
 Heavy Duty
2,500 KG Capacity50/75mm Pitch
Explore our high-performance modular storage assemblies, designed for maximum volumetric efficiency, cold-chain thermal retention, and automated SKU selective retrieval.
Heavy Duty
 Custom CAD
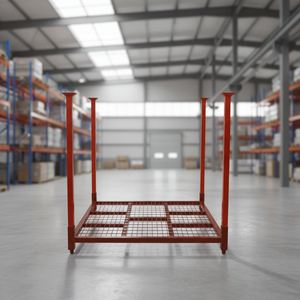 Stackable
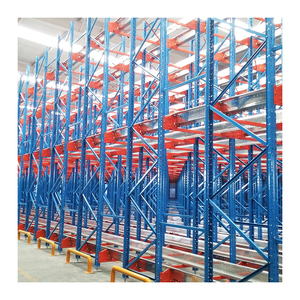 Automated
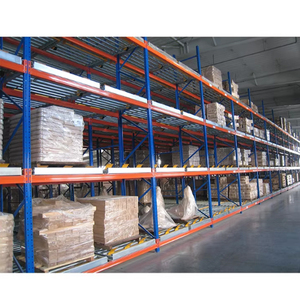 Gravity Flow
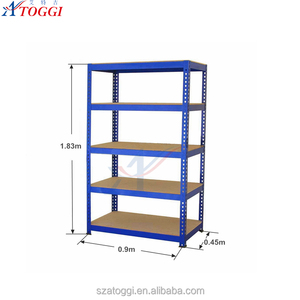 Modular Mobile
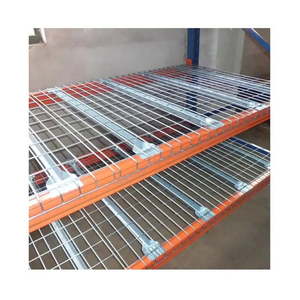 Galvanized
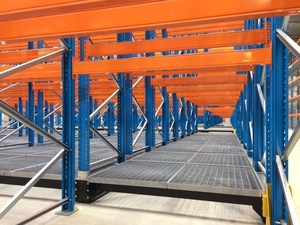 Max Volume
In modern logistics real estate, the skyrocketing cost per square foot demands exceptional volumetric yield. Movable pallet racking (frequently designated as motorized mobile racking, compactor pallet bases, or mobile heavy-duty sliding racks) represents an elite mechanical engineering approach that eliminates dead static aisle space. By mounting heavy-duty selective rack superstructures onto electronically synchronized motorized bogies traveling on floor-embedded guide tracks, this dynamic configuration requires only one working aisle to service multiple blocks of racks.
Conventional static selective racking allocates up to 60% of total facility footprint solely to forklift access corridors. In contrast, an OEM/ODM engineered movable pallet racking solution increases pallet storage density by 80% to 100% within the same physical perimeter, while sustaining 100% random pallet selectivity. Each mobile carriage is guided by precision laser safety grids, photoelectric stop switches, and dynamic variable-frequency drive (VFD) controls, guaranteeing zero cargo vibration during carriage transit even when handling loads up to 30 tons per bay.
Engineered strictly using prime certified Q235B and Q355B cold-formed structural steel, delivering superior tensile strength and minimum elastic deflection under extreme static loads.
Integrated infrared presence sensors, longitudinal emergency trip bars, acoustic warning alarms, and seismic locking devices comply with European EN 15095 safety standards.
Advanced automated 10-step surface finishing incorporates continuous acid pickling, phosphating, and electrostatic powder curing to guarantee zero corrosion in cold freezers or humid environments.
Custom fabricated chassis, custom drive ratios, PLC communication interfaces (Siemens / Mitsubishi), and bespoke track embedment designs engineered to client structural slab criteria.
| Storage System Architecture | Floor Space Utilization | Direct Pallet Accessibility | Cold-Chain Operating ROI | Seismic & Dynamic Stability |
|---|---|---|---|---|
| Movable Pallet Racking (Electric Mobile) | 85% – 90% (Ultra High) | 100% (Individual Open-Aisle Selectivity) | Maximum (Cuts refrigerated footprint by 50%) | High (Interlocked chassis with anchor guide rails) |
| Conventional Selective Racking | 35% – 40% (Aisle-Heavy) | 100% (Direct Instant Access) | Low (Large refrigerated air loss in corridors) | Standard Floor Anchored |
| Drive-In / Drive-Through Systems | 65% – 75% (High Density) | Low (Strict LIFO / Last-In First-Out) | Moderate (Forklift collision hazard in lanes) | Vulnerable to internal mast impacts |
| Radio Shuttle Automated Racks | 75% – 85% (High Density) | Channel Batched (Semi-Automated) | High (Fast deep-lane channel throughput) | Rigid high-density bracing |
B2B supply chain architects and procurement executives must evaluate intralogistics infrastructure not merely as capital assets, but as dynamic energy-conservation mechanisms. The integration of high-density mobile racking is accelerating across high-value cold storage, pharmaceutical warehousing, industrial manufacturing, and cross-border distribution centers due to several transformational industry trends:
Refrigerated cubic volume is the single most expensive operating expense in temperature-controlled logistics (-25°C to -40°C). By eliminating excess aisles, movable pallet systems shrink the thermal envelope required to store identical tonnage, yielding documented refrigeration electrical savings of up to 40% per annum.
Modern procurement mandates real-time protocol integration. Emerging mobile racking platforms leverage decentralized IoT sensors and Ethernet/IP protocols connecting directly with tier-1 Warehouse Management Systems (WMS). Aisles open automatically via automated forklift dispatch signals or AGV routing prior to vehicle arrival, eliminating operator cycle waiting times.
International building codes (including IBC, Eurocode 3, and AS 4084) enforce rigorous horizontal acceleration tolerances in seismic zones like the Philippines, Indonesia, and the Pacific Rim. Contemporary OEM factories deploy anti-tipping guide rails, laser track level calibrations down to 1mm tolerances, and continuous high-yield roll-formed upright sections.
When specifying movable storage components via an OEM/ODM partner, procurement leaders must audit steel mechanical test certs (MTC), motor drive duty cycle ratings, PLC system fault redundancy, and the availability of precision track alignment surveying tools before placing manufacturing deposits.
Since 2001, Guangzhou Heda Shelves Co., Ltd. has established an authoritative footprint as a leading global manufacturer and exporter of certified industrial storage systems, serving clients in over 120 countries. Operating from a modern 30,000 square meter factory base with a robust technical force of over 300 experienced specialists, we maintain a monthly manufacturing capacity reaching 30,000 tons of prime engineered steel racking.
Strict third-party compliance holding official CE Certificate No. 2435-CPR-8605159 and ISO 9001:2015 Quality Management No. 18624Q00169R0M.
Strategically situated in South China port hubs (Guangzhou / Nansha), ensuring rapid direct shipment: 2-5 days to Vietnam/Philippines, 5-7 days to Singapore/Thailand, and 7-10 days to Indonesia.
Our dedicated senior structural engineering team delivers free custom warehouse CAD layout plans, comprehensive structural load calculations, and full 3D visual renderings within 24 hours.
10 fully monitored production phases: continuous coil uncoiling, precision slitting, cold roll-forming, automatic punching, robotic welding, acid phosphating, and uniform electro-coating.
Send our senior engineering group your warehouse architectural DWG drawings, pallet load constraints, and forklift specs for a full custom project proposal with structural stress analysis.
Comprehensive engineering, civil works, and overseas logistics answers for industrial supply chain decision-makers.
Movable pallet racking relies on precision guided wheel bogies traveling on floor-embedded rails. The warehouse concrete floor requires minimum load-bearing capacity designed for concentrated wheel loads (often exceeding C25/C30 grade concrete). Floor levelness must adhere to DIN 18202 standards (typically within ±1.5 mm to 2 mm deviation across 2-meter track centers). Guide tracks can be placed into recessed trenches during the initial building slab pour or retrofitted by saw-cutting existing slabs followed by non-shrink secondary grouting.
Our mobile bases integrate a triple-redundant European safety matrix compliant with EN 15095 directives. Longitudinal optical light curtains sweep active aisles, automatically halting carriage motors within 100 milliseconds if any pedestrian or forklift enters. Full-length physical trip kick-bars along the bottom carriage frames halt motion upon physical touch. Emergency mushroom stop consoles are positioned on every mobile rack facade, accompanied by synchronous audible klaxons and revolving LED strobes.
Yes, our systems are widely utilized in cold chain and frozen seafood warehouses down to -30°C. For sub-zero operations, we equip electric carriages with low-temperature synthetic lubricants, silicone wiring harnesses rated for -40°C, internal anti-condensation electrical cabinet heaters, and cold-resistant gear motors. The compaction reduces refrigerated chamber cubic footprint by up to 50%, generating dramatic annual electricity cost savings.
Mobile carriage bases feature dual contingency mechanisms. In standard deployments, control panels can be seamlessly wired into local emergency backup diesel generators. In facilities without emergency generator backup, manual mechanical release levers allow warehouse operators to disengage electro-magnetic brakes and hand-crank the carriages to expose a crucial aisle for emergency stock extraction.
As a specialized high-capacity manufacturer, we tailor upright column profiles (80mm to 140mm width), steel gauges (1.8mm to 3.0mm Q235B/Q355B steel), beam section depths (80mm to 160mm box beams), carriage chassis lengths (up to 40+ meters continuous), and motor horsepower. We provide private-label branding, customized RAL powder-coat color schemes matching your corporate identity, custom PLC programming, and comprehensive English installation manuals.
Standard OEM production runs take 20 to 30 working days from approval of engineering CAD drawings. Every structural upright and beam bundle is protected with bubble wrap, corrugated cardboard strapping, and steel skid dunnage engineered for standard 40HQ sea containers. Mobile motorized bases and electronic control consoles are packed in treated fumigation-free plywood crates to ensure corrosion-free trans-oceanic voyage.