Engineered from premium cold-rolled Q235B/Q355B structural steel, conforming strictly to CE, ISO 9001:2015, and FEM 10.2.02 international load tolerances.
A technical examination of volumetric footprint optimization, structural steel elasticity, and material handling kinematics for modern industrial facilities.
In the modern era of high-velocity logistics, escalation of industrial land values, and the skyrocketing square-meter utility costs in cold-storage and urban distribution hubs, warehouse managers can no longer rely on conventional 2.5-meter to 3.2-meter wide selective aisles. High-Density Pallet Racking (HDPR) engineering represents the structural bridge between conventional floor storage and fully automated AS/RS matrix grids. By collapsing dynamic access aisles into continuous storage blocks, engineering systems such as Drive-In, Drive-Through, Radio Shuttle Racking, Push Back, and Gravity Pallet Flow can drive warehouse cubic space utilization from an average of 42% up to an astonishing 85%.
For every square meter converted from transit aisles into active pallet positions, the amortized cost per pallet drop diminishes by 22% to 37% over a five-year operating lifecycle. However, spatial compression introduces significant engineering trade-offs: structural beam deflection limits, dynamic forklift impact variables, torsional frame stability, and pallet selectivity kinematics.
Utilizing high-tensile cantilevered galvanized guide rails, semi-automated lithium-powered radio shuttles navigate deep storage bays up to 40 pallets deep. Eliminates forklift rack ingress, reducing frame impact structural fatigue by over 92% while delivering rapid automated indexing for both FIFO and LIFO modes.
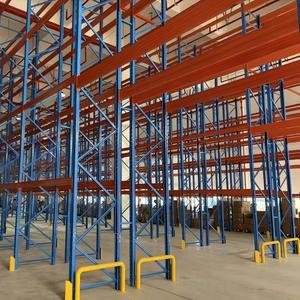
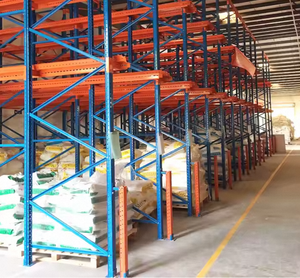
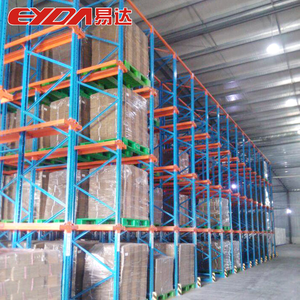
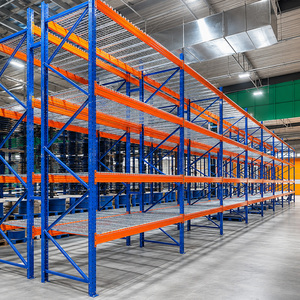
Engineered for high-volume, low-SKU inventory batching. Structural upright frames feature continuous cold-rolled cantilevered brackets supporting heavy-gauge steel pallet rails. Forklifts enter racking channels directly, making it the most cost-effective structural solution for FMCG, cold storage, and chemical drum logistics.
Dynamic mechanical storage utilizing inclined roller beds (Gravity Flow - FIFO) or nested telescoping steel carts on inclined structural channels (Push Back - LIFO). Gravity-driven mechanics optimize pick faces automatically without electronic controls, ideal for temperature-controlled food distribution and pharmaceuticals.
| Racking Architecture | Space Density | Selectivity | Load Limit (Per Pallet) | Forklift Damage Risk | Throughput Velocity | Ideal Inventory Profile |
|---|---|---|---|---|---|---|
| Radio Shuttle System | Ultra High (85%) | Lane Selective | 500 - 2,000 kg | Extremely Low | Fast (Automatic) | Cold Storage, Food Export, FMCG Hubs |
| Drive-In / Drive-Through | High (75%) | Last In First Out | 800 - 1,800 kg | Moderate to High | Standard (Manual) | Beverage, Agriculture, Raw Steel Coils |
| Push Back Racking (2-6 Deep) | Medium-High (65%) | LIFO Per Channel | 500 - 1,500 kg | Low | Fast (Gravity Fed) | Buffer Storage, Automotive Assemblies |
| Gravity Pallet Flow | High (80%) | Strict FIFO | 300 - 1,500 kg | Low | Ultra Fast (Gravity) | Perishables, Pharmaceuticals, Date-Coded |
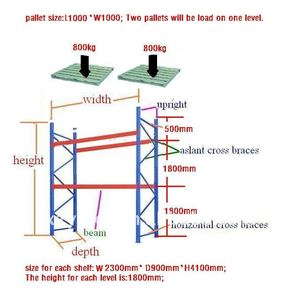
| Heavy Selective Pallet Rack | Standard (45%) | 100% Direct | 1,000 - 5,000 kg | Low (Wide Aisles) | High Flexibility | 3PL Warehouses, Multi-SKU E-Commerce |
Strategic structural adaptations driven by seismic compliance, robotic automation interfaces, ESG cold-chain decarbonization, and advanced material metallurgy.
Procurement directors are rapidly shifting away from isolated static racking toward "Automation-Ready" infrastructure. Modern high-density installations are engineered with precision ground guide angles, laser-reflective upright positioning, and reinforced bottom beam levels that allow seamless docking for Autonomous Mobile Robots (AMRs) and automatic guided counterbalance trucks. Specifying ISO-standard aisle tolerances and precision floor deflections during initial racking procurement prevents costly retrofits when automated logistics phases are launched.
With massive supply chain decentralization across the Pacific Rim, ASEAN (Indonesia, Philippines), and the Americas, static load calculations are no longer sufficient. International tenders mandate compliance with RMI MH16.1 (USA), AS 4084 (Australia), and EN 15512 (Europe) seismic dissipation design. Suppliers are utilizing custom micro-alloyed hot-rolled structural steel coils (such as Q355B and high-yield cold-rolled profiles) coupled with engineered flared baseplates, heavy back-to-back cross bracings, and M16/M20 chemical concrete anchors to absorb base shear acceleration without catastrophic structural buckling.
The global perishable foods, biological vaccines, and refrigerated seafood sectors are witnessing an unprecedented boom. Because cold-chain sub-zero facilities (-25°C to -30°C) incur exorbitant operational refrigeration overheads, cubic volume utilization dictates business survival. Radio Shuttle Racking and Drive-In Systems represent over 68% of new cold-storage racking procurement. Metallurgical specifications in these tenders require impact-tested steel exhibiting zero ductile-to-brittle transition at cryogenic temperatures, alongside heavy hot-dip galvanized finishes that prevent oxidation from thermal dew condensation cycles.
Environmental social governance (ESG) compliance has made toxic chromate pre-treatments obsolete. Tier-1 Chinese manufacturers now lead international compliance through multi-stage zirconium or silane surface passivation followed by non-VOC TGIC-free electrostatic polyester epoxy powder coating. The resulting finish withstands 500+ hours of ASTM B117 cyclic salt-spray tests, ensuring high chemical resilience against agricultural fertilizers, industrial battery acids, and humid equatorial logistics climates.
Founded in 2001, providing 25+ years of verified structural racking engineering, precision roll-forming manufacturing, and direct maritime logistics execution.
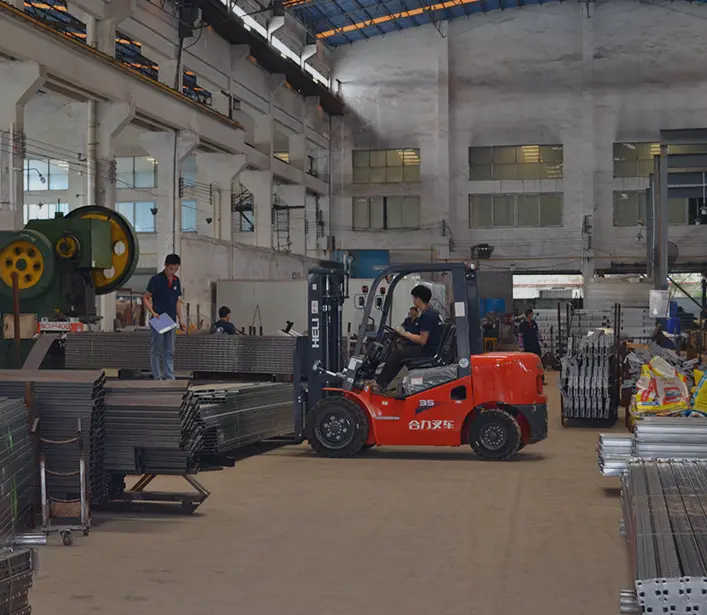
Guangzhou Heda Shelves Co., Ltd. stands as one of China's premier heavy industrial storage and mezzanine manufacturing conglomerates. Operating out of our modern 30,000 m² integrated production base in South China, our facility maintains an ultra-high production volume exceeding 30,000 metric tons per month, backed by an elite engineering and fabrication corps of over 300 experienced specialists.
Unlike trading intermediaries, HEDA Shelves executes end-to-end industrial control: from raw steel coil slitting and automated CNC multi-station hole punching to robotic welding, continuous cold roll profiling, 10-stage chemical pre-treatment, and international logistics packing. Our prime maritime positioning near Guangzhou and Nansha ports provides unprecedented freight transit advantages (2–5 days to Vietnam, 3–5 days to Manila, 5–7 days to Singapore/Thailand, and 7–10 days to Jakarta).
Complete regulatory compliance with international tenders. Holder of CE Certificate No. 2435-CPR-8605159, ISO 9001:2015 Quality Management No. 18624Q00169R0M, and comprehensive RoHS chemical safety accreditations.
Our dedicated structural engineering division delivers preliminary CAD warehouse layout blueprints, spatial density simulations, and 3D isometric structural renderings within 24–48 hours, free of contractual obligation.
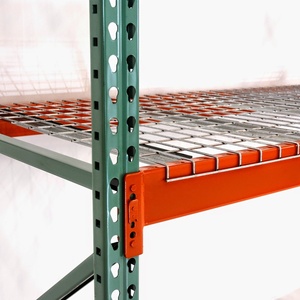
From custom beam connectors, drop-in teardrop pin specifications, wire mesh decking, to customized high-capacity structural steel mezzanines (300 to 1,000 kg/m²), we tailor dimensions, steel gauges, and corporate brand colors.
Every beam, upright column, and horizontal brace is precisely bundled, strapped, and corner-protected to maximize standard 20GP, 40GP, and 40HQ container volumetric capacity, dramatically slashing oceanic freight cost per pallet drop.
From prime Q235B cold-rolled steel coils to high-temperature curing ovens, quality is verified at every station.
Mill test certificates (MTC) verified for tensile yield & chemical composition.
Automated slitting lines cutting strip steel with ±0.2mm lateral precision.
High-speed mechanical CNC punches punch teardrop or 75mm pitch upright holes.
Multi-stand continuous roll lines forming complex 12-fold structural profiles.
Robotic CO2 gas shielded arc welding securing connectors with high penetration.
Removal of weld spatter, burrs, and flash for absolute structural smoothness.
Deep acid bath immersion removing surface scale, iron oxides, and oil residues.
Micro-crystalline phosphate conversion coating applied for chemical bonding.
Electrostatic spray guns applying 60-80μm durable pure polyester resin powder.
200°C thermal baking tunnel curing followed by laser dimension & load check.
Expert answers addressing the most critical technical, commercial, structural, and regulatory concerns voiced by warehouse directors and procurement specialists.
Submit your facility dimensions, ceiling clearances, and pallet loading parameters today. Our senior engineering team will design a fully compliant CAD layout and deliver an itemized factory-direct investment quotation within 24 hours.